
Engineered to international civil defense, ASTM, and EN standards. Browse core profile configurations, walk-in cold envelope panels, and digital management terminals.
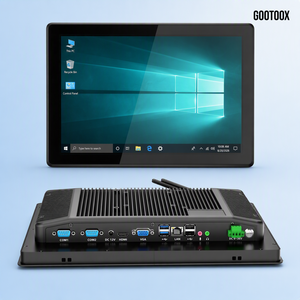
IP65 sealed fanless monitoring terminal engineered for low-temperature automated atmospheric cold stores and food logistics control.
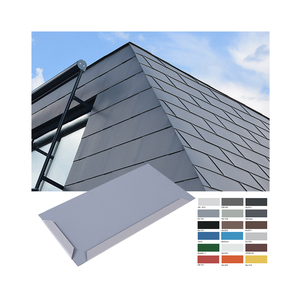
AZ150 Galvalume coating with baked fluoropolymer (PVDF) finish for maximum corrosion resistance in coastal and high-UV environments.
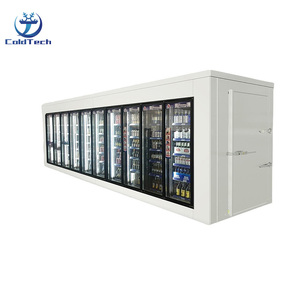
PIR/PUR insulated perimeter frame with heated anti-condensation dual-pane tempered glass for commercial bakery and retail cold distribution.
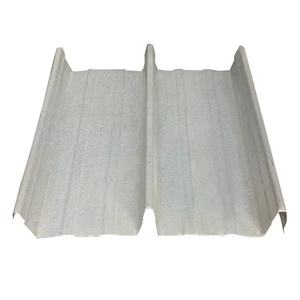
Deep ribbed structural load profile utilizing high-yield DX51D galvanized base steel for extreme industrial wind load and rain shed resistance.
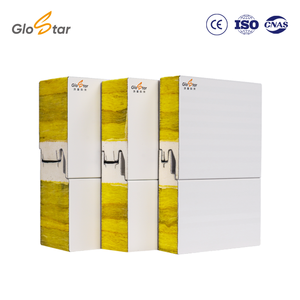
Non-combustible bonded mineral glass wool core with tongue-and-groove jointing, ensuring up to 120-minute passive fire barrier performance.
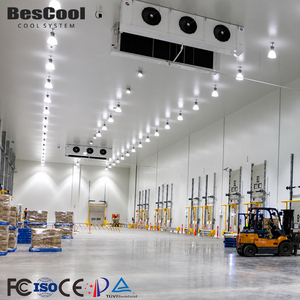
Continuous cyclopentane-blown PIR panels up to 200mm thickness for cold storage warehouses requiring strict -25°C to -40°C temperature stability.
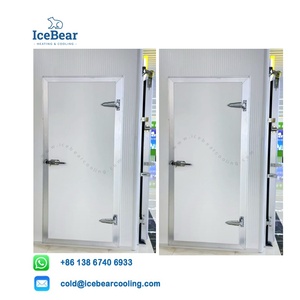
Heavy-gauge aluminum structural frames fitted with self-regulating perimeter heating cables, preventing frost build-up in high-traffic logistics bays.
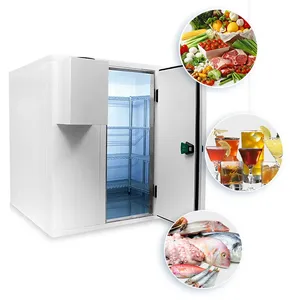
Prefabricated cam-lock panelized cold storage structure with integrated monoblock condensing unit for fast field deployment in remote operations.
The modern building envelope has evolved from a passive rainscreen into an engineered structural barrier that dictates building life-cycle carbon emissions, structural thermal bridging, acoustic isolation, and life-safety fire resistance. Within this landscape, leading Chinese steel cladding manufacturers have established global manufacturing benchmarks through vertical integration—from hot-dip galvanizing lines and metallurgical coil coating to automated high-speed continuous double-belt polyurethane/polyisocyanurate (PIR) and mineral wool panel production.
Unlike fragmented regional processors, premier tier-1 Chinese factories operate fully automated continuous manufacturing lines featuring four-component high-pressure cyclopentane foaming injection systems, precision laser cutting, and in-line auto-tracking profiling routers. These facilities deliver strict dimensional tolerances (±0.5 mm in cross-sectional profile, ≤1 mm across a 12-meter panel span) while dramatically reducing delamination risks through high-yield polyurethane reactive polyurethane (PUR-hot-melt) structural bonding agents.
Value Insight for Procurement Engineers: Sourcing directly from tier-1 Chinese production hubs gives EPC contractors and structural engineers an estimated 28% to 42% cost efficiency per square meter over North American and Western European equivalents, while matching or exceeding ASTM A792 (AZ150 Galvalume), EN 14509 (Self-supporting double-skin insulated sandwich panels), and FM Global 4880/4881 standards for external fire exposure and wind uplift resistance.
A rigorous metallurgical and thermodynamic reference for consulting engineers, detailing physical characteristics, failure points, and specific application criteria.
| Panel Core / Specification | Thermal Cond. (λ) | Density Range | Fire Behavior & Index | Compressive Modulus | Primary Industrial Application |
|---|---|---|---|---|---|
| PIR (Polyisocyanurate) Cyclopentane micro-cell blowing |
0.019 – 0.022 W/m·K | 40 – 45 kg/m³ | B-s1,d0 / ASTM E84 Class A Self-extinguishing char barrier |
≥ 140 kPa | Cold storage distribution hubs, temperature-controlled logistics, energy-efficient commercial roofs. |
| Hydrophobic Rockwool Basalt spun fiber matrix |
0.038 – 0.044 W/m·K | 100 – 140 kg/m³ | A1 Non-Combustible Melting point > 1000°C |
≥ 100 kPa | Fire-rated compartment walls, petrochemical facilities, high-occupancy manufacturing zones, acoustic partitions. |
| Glass Wool Composite Elastic silane-treated fibers |
0.034 – 0.038 W/m·K | 50 – 65 kg/m³ | A1 Non-Combustible Zero toxic gas emission |
≥ 70 kPa | Auditoriums, airport hangars, modular steel workshops requiring high acoustic absorption (NRC ≥ 0.85). |
| PUR (Rigid Polyurethane) Polyol-isocyanate crosslinked |
0.022 – 0.026 W/m·K | 38 – 42 kg/m³ | B2 / DIN 4102 Combustible without firebreak |
≥ 130 kPa | Standard chillers, general agricultural sheds, economy temperature-regulated processing lines. |
| PPGI / PPGL Galvalume Skin 55% Al, 43.4% Zn, 1.6% Si alloy |
50 W/m·K (Metal Skin) | 0.4 – 0.8 mm thk | Class 0 Surface Spread Non-combustible face |
Yield: ≥ 300 – 550 MPa | Exterior weather skins, high-UV desert envelopes, marine littoral environments within 3 km of shoreline. |
*Note: Tested according to ASTM C518, EN 13165, and ISO 8301. Exact acoustic attenuation (STC) ranges between 29 dB to 38 dB based on core density and micro-ribbed steel skin profile selection.
Key technological, regulatory, and environmental shifts guiding international procurement decisions for modern capital projects.
Standard hot-dip galvanizing (Z275) is quickly being replaced by Zn-Al-Mg coatings (containing 3% Mg and 2-3% Al). ZAM forms a dense, self-healing simonkolleite barrier over exposed laser-cut edges and drilled fastener holes, outperforming standard galvanized steel by 4-5 times in aggressive salt-spray (ASTM B117) exposure.
With the European Union Carbon Border Adjustment Mechanism (CBAM) and global Scope 3 emissions mandates, Chinese tier-1 mills are shifting to scrap-based Electric Arc Furnaces (EAF) and hydrogen-reduced direct iron making. Buyers are increasingly requesting third-party verified Environmental Product Declarations (EPD) to secure LEED Platinum and BREEAM green building certifications.
Architects and project owners are moving away from secondary ballast-mounted solar frames toward single-step structural BIPV roof panels. Specialized sandwich panels with standing-seam ribs or embedded crystalline modules integrate mechanical fastening without penetrations, preserving thermal envelope integrity while reducing overall structural dead load.
Traditional exposed through-fix screws represent prime failure points for water ingress and thermal bridges. Sourcing preferences have heavily tilted toward concealed-fix interlocking secret-joint panels. These incorporate factory-foamed EPDM air-seals and integrated thermal break gaskets to maintain envelope airtightness across high structural wind differentials.
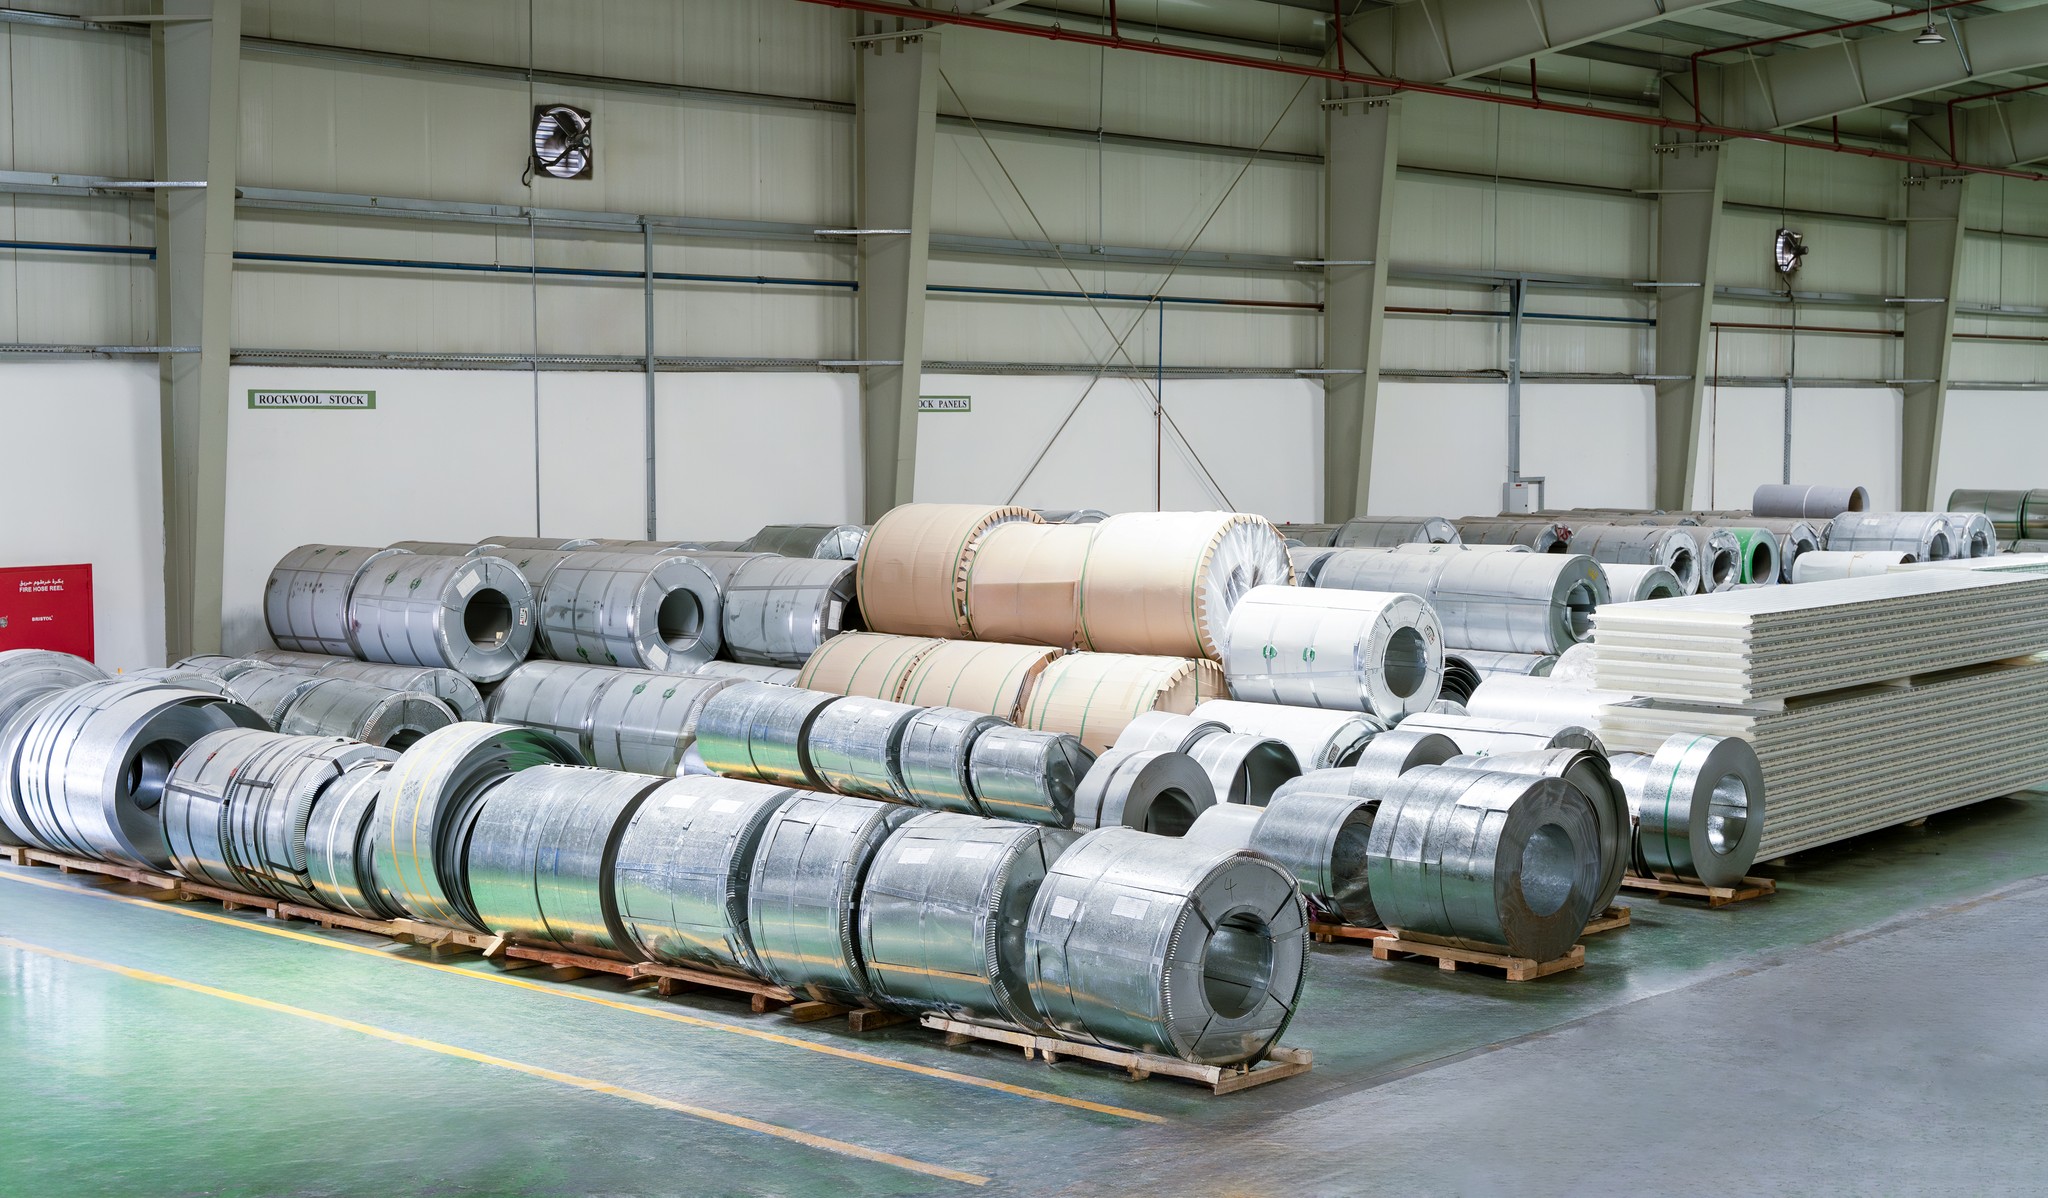
Procuring from an established Chinese manufacturer guarantees advanced metallurgical control and consistent assembly line quality. Leading operations combine continuous continuous roll forming, automated high-pressure multi-component metering, and continuous double-caterpillar heating conveyors extending over 35 meters in length. This long curing chamber guarantees complete polyurethane polymerization and eliminates internal stress concentrations that cause surface waviness or "oil-canning."
In-depth engineering answers addressing compliance, quality verification, logistics packaging, and life-cycle performance.
Compliance is achieved by tailoring the chemical formulation to maintain an isocyanate-to-polyol index exceeding 250 (PIR index). Under heat exposure, this cross-linked chemical structure forms a high-density polyisocyanurate char ring that blocks oxygen transfer, preventing self-sustaining combustion and meeting flame-spread indices ≤ 25 with smoke-developed indices ≤ 450.
Oil-canning (visible surface waviness) is mitigated through three controls: (1) using minimum 0.5 mm to 0.6 mm steel skin thickness; (2) incorporating micro-ribbing, pencil ribbing, or embossed striations across the face to increase the moment of inertia; and (3) using continuous double-belt laminators that apply uniform, heated mechanical pressure during the core's exothermic reaction.
For installations within 3 km of seawater or inside heavy chemical industrial corridors, standard PE (polyester) coatings are insufficient. Specifications should mandate PVDF (Polyvinylidene Fluoride, 70/30 Kynar 500 formulation) or HDP (High-Durable Polyester) coatings applied over an AZ150 Galvalume (55% Al-Zn) or SuperDyma (Zn-Al-Mg) substrate, with a total dry film thickness (DFT) ≥ 28μm.
Panels are stacked with protective, low-tack self-adhesive PE films, side-edge protective cardboard corner guards, and wrapped in heavy-duty polyethylene shrink wrap. Bundles are loaded onto tailored timber pallets or heavy-gauge steel skids with nylon lifting slings, secured in 40ft High Cube (HC) or Open Top containers to prevent transit friction, moisture condensation, or crane damage during intermodal handling.
Cold chain envelope panels utilize a labyrinth dry-joint tongue-and-groove or specialized cam-lock mechanical connector with dual-track compressible PVC/EPDM sealing beads. The core-to-core interface eliminates all through-metal contact between internal and external skins, preventing condensation, frost formation, and parasitic refrigeration load losses.
Standard profile and standard RAL color runs typically carry an MOQ of 500 to 1,000 square meters, with automated plant production completed in 7 to 14 days. Custom widths, specialized non-standard coil thicknesses (e.g., 0.8 mm), or specialized coatings (PVDF metallic finishes) require a mill run coil MOQ of approximately 3,000 square meters and a 20 to 25-day manufacturing lead time.
Send your bill of quantities (BOQ), structural purlin layout, wind load design criteria, or thermal envelope requirements to our technical engineering team for certified calculations, complete CAD connection details, and competitive ex-factory pricing.
Our sales engineers respond to project questions during working hours (GST+4).