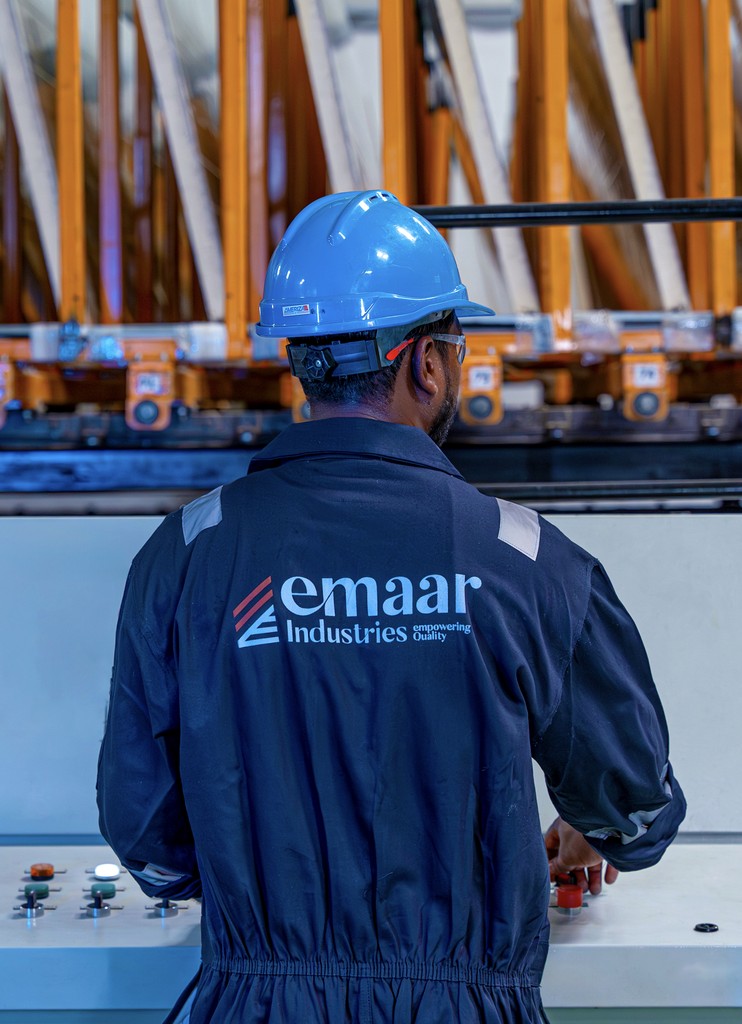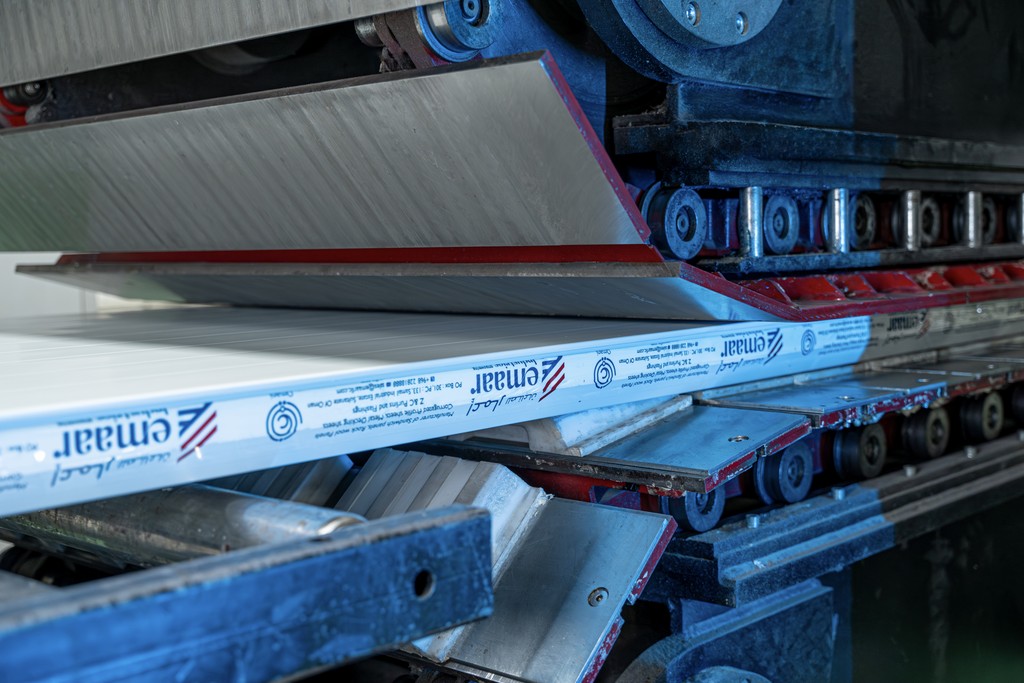
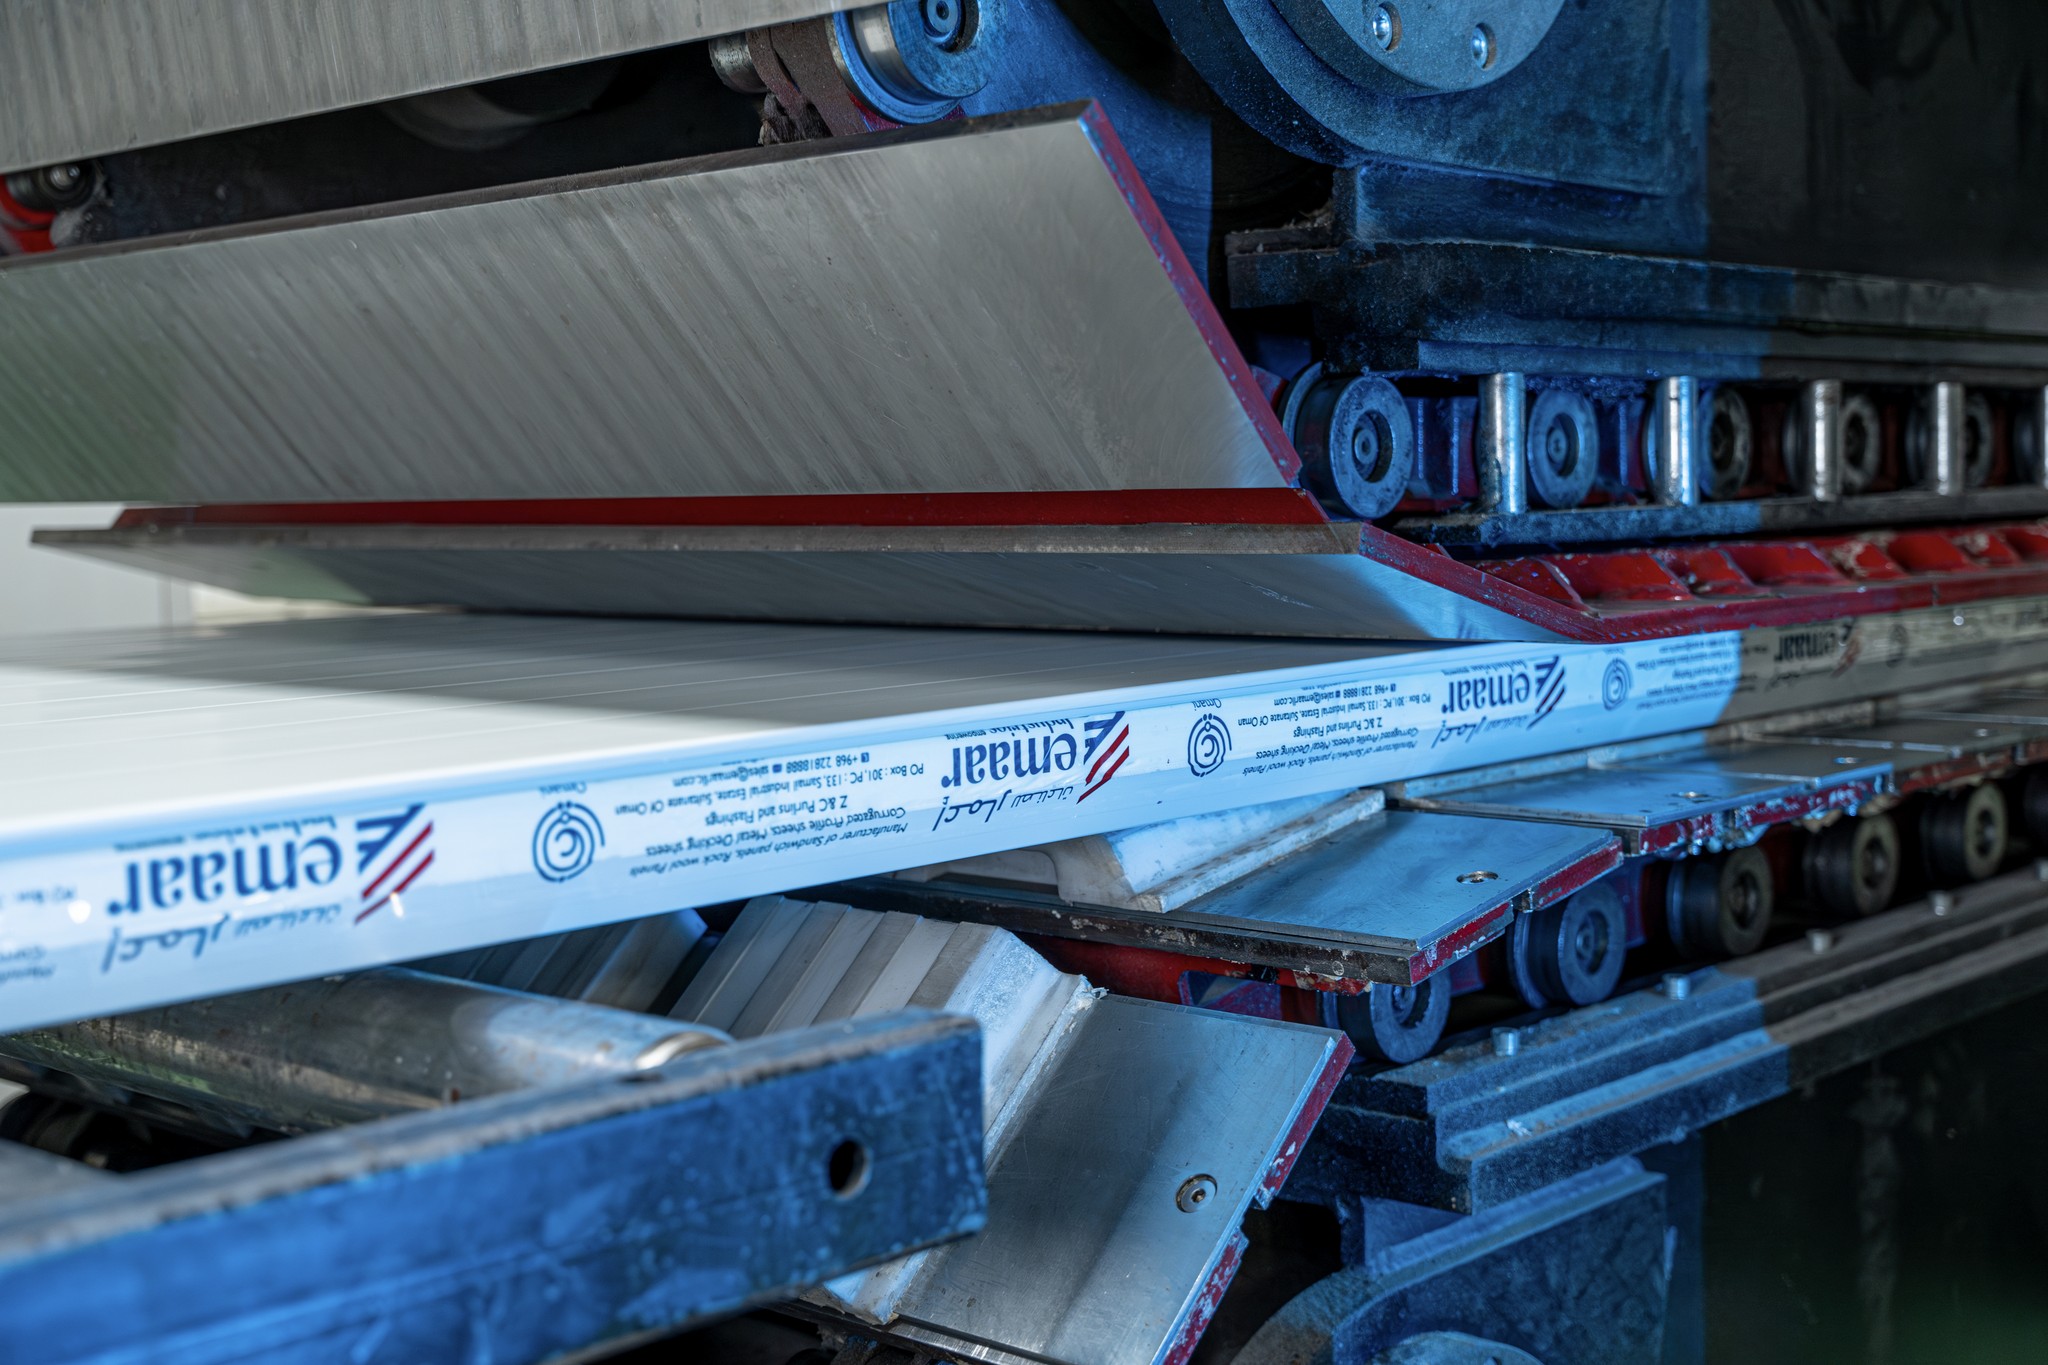
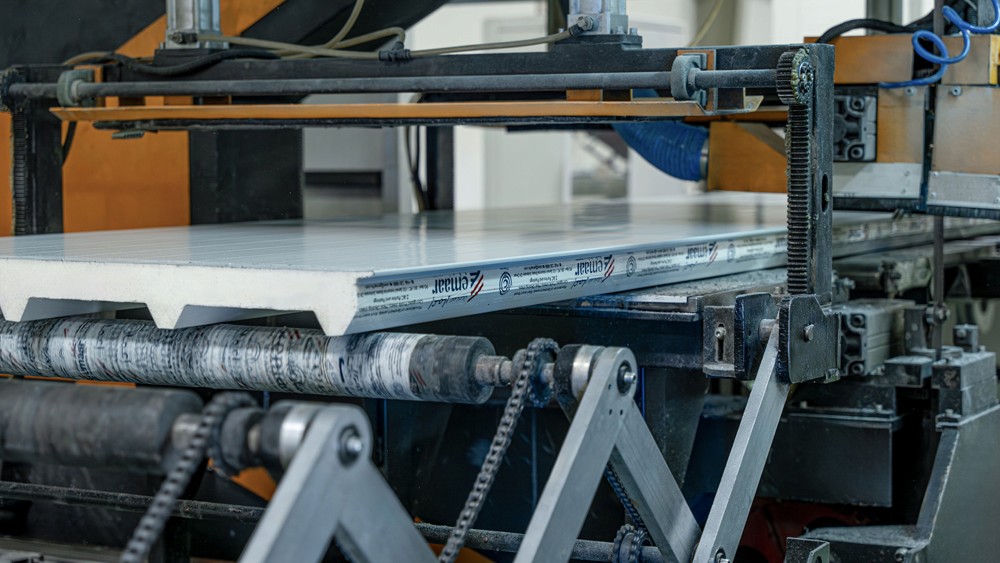
High speed CNC cold rolled Z purlins roll-forming line at Emaar Industries Muscat facility
Industrial warehouse roof framing constructed with galvanized cold rolled Z purlins
Quality inspection and laser tolerance verification of cold formed steel sections
Pre-engineered building structural envelope using continuous lap Z purlins
0
Min. Yield Strength (S450GD Grade)
0
Steel Weight Savings via Continuous Lap
0
Structural Projects Across GCC & Africa
0
Hot-Dip Galvanized Zinc Coating (Z275)
Structural Excellence · High-Tensile Steel Engineering

Cold Rolled Z Purlins: Continuous Lap Optimization, Technical Standards & Global Sourcing

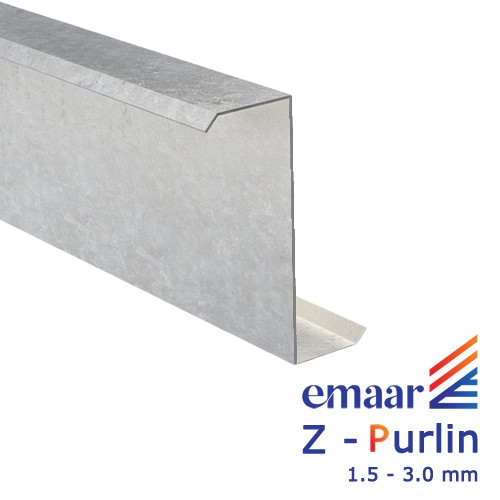
In contemporary pre-engineered buildings (PEBs), heavy industrial warehouses, and large-span solar substructures, cold rolled Z purlins represent the pinnacle of structural secondary framing efficiency. Unlike standard single-span cold-formed channels, cold rolled Z purlins are engineered with asymmetric flanges—specifically manufactured with unequal widths (typically a wider flange of 64 mm and a narrower flange of 58 mm)—which enable identical profiles to nest snugly inside one another at rafter support points. This structural lapping configuration transforms isolated, simply supported beams into an integrated, continuous structural beam system across multi-bay portal frames.

Manufactured at Emaar Industries' advanced roll-forming facility in Muscat, Oman, our cold-formed Z sections are roll-formed from prime, certified high-yield structural steel coils complying strictly with BS EN 10346 (S350GD, S390GD, S450GD) and ASTM A653M Grade 50/80 standards. By doubling the effective section modulus over peak negative bending moment zones at frame rafters, our continuous lapped Z purlin systems reduce total structural steel consumption by up to 25% to 35% while suppressing vertical and lateral-torsional deflection under extreme aerodynamic uplift, dynamic sand accumulation, and thermal shock conditions typical of the Arabian Gulf and equatorial Africa.

Engineering Data & Load Capacities

Standard Dimensional Matrix & Continuous Lap Section Properties

Cold-formed Z sections provide an exceptional strength-to-weight ratio. The intentional differential between the top and bottom flange widths (5 mm to 8 mm difference) allows for seamless nestable overlaps directly across rafter cleats, providing double section properties across high-shear negative moment regions.

Profile Model Web Depth (D mm) Flange Dimensions (F1 / F2 mm) Lip Length (L mm) Available Thickness (mm) Steel Grades (Yield Strength) Protective Coating Mass
EZ-150 Series 150 64 / 58 (Asymmetric Nesting) 18 – 20 1.50, 1.80, 2.00, 2.50 S350GD (350 MPa) / ASTM A653 Gr 50 Z275 (275 g/m²) or AZ150 Galvalume
EZ-200 Series 200 68 / 62 (Asymmetric Nesting) 20 – 22 1.80, 2.00, 2.50, 3.00 S350GD, S450GD (450 MPa) Z275 Hot-Dip Galvanized / ZAM
EZ-250 Series 250 74 / 66 (Asymmetric Nesting) 22 – 24 2.00, 2.50, 3.00, 3.20 S350GD, S450GD (450 MPa) Z275 to Z350 Heavy Galvanized
EZ-300 Series 300 85 / 75 (Heavy Duty Span) 25 – 28 2.50, 3.00, 3.20 S450GD, ASTM A653 Gr 80 (550 MPa) Z275 Zinc / Coastal Protective System
EZ-350 Heavy Span 350 95 / 85 (Ultra-Wide Flange) 28 – 30 2.50, 3.00, 3.20, 3.50 S450GD (450 MPa) Z275 / Marine Class Salt Spray Rated

* Custom dimensions, unequal web depths, and specialized flange return lip angles are configurable on our automated CNC roll-forming lines. Every order is provided with EN 10204 Type 3.1 Mill Test Certificates.

Structural Mechanical Gain

Why Continuous Lap Design Eliminates 30% Structural Steel Weight

Designing purlins as continuous multi-span members rather than isolated simple beams transforms the internal bending moment diagram. Over intermediate rafter supports, the overlapping Z sections act as a unified double-thickness composite section, resisting peak negative moments while dramatically reducing mid-span deflection.

Optimal Lap Ratio (10% to 15%)Continuous lap lengths equal to 0.10 to 0.15 of the frame bay span ensure total structural moment continuity without localized flexural failure.
Mid-Span Bending ReliefNegative bending moments over supports relieve sagging moments at mid-span, allowing thinner steel gauges over wide 8m to 10m column bays.
Double Shear ResistanceNested web layers at bolt locations double the bearing capacity and bolt pull-through resistance against extreme aerodynamic wind uplift.
Thermal Expansion ToleranceInline slotted punch connections (14x22 mm) absorb extensive thermal cycling without inducing catastrophic buckling stresses in extreme climates.
Muscat Manufacturing Hub

Why Tier-1 EPC Contractors Partner with Emaar Industries

Headquartered in Al Khuwair, Muscat, Emaar Industries operates as an integrated manufacturing powerhouse delivering heavy-duty envelope and structural secondary steel components across the Middle East and Africa. Over 550 industrial facilities, logistics parks, power stations, and agro-storage hubs have been built using our structural cold-formed profiles and insulated building envelopes.

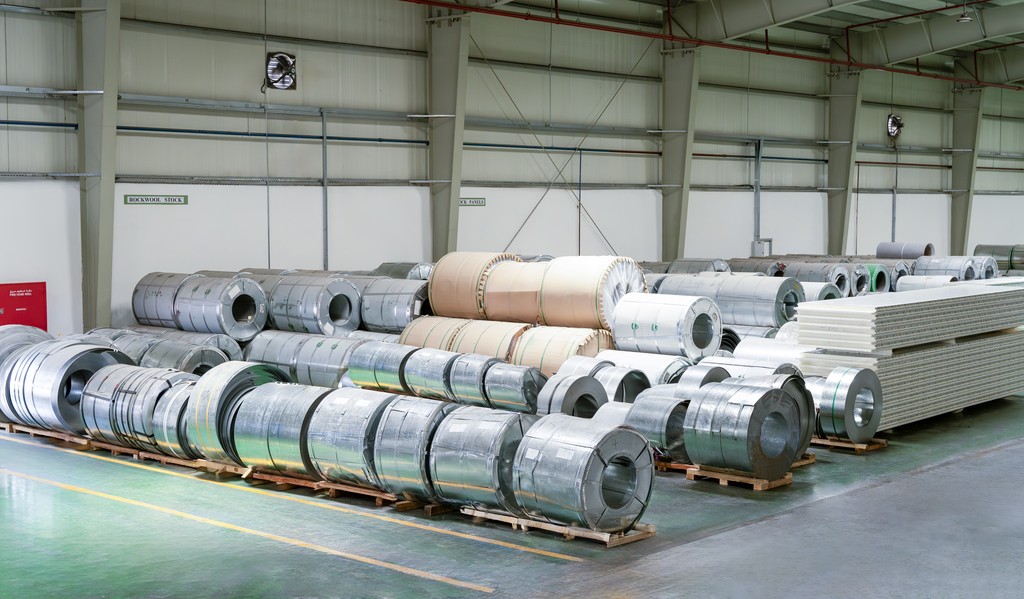
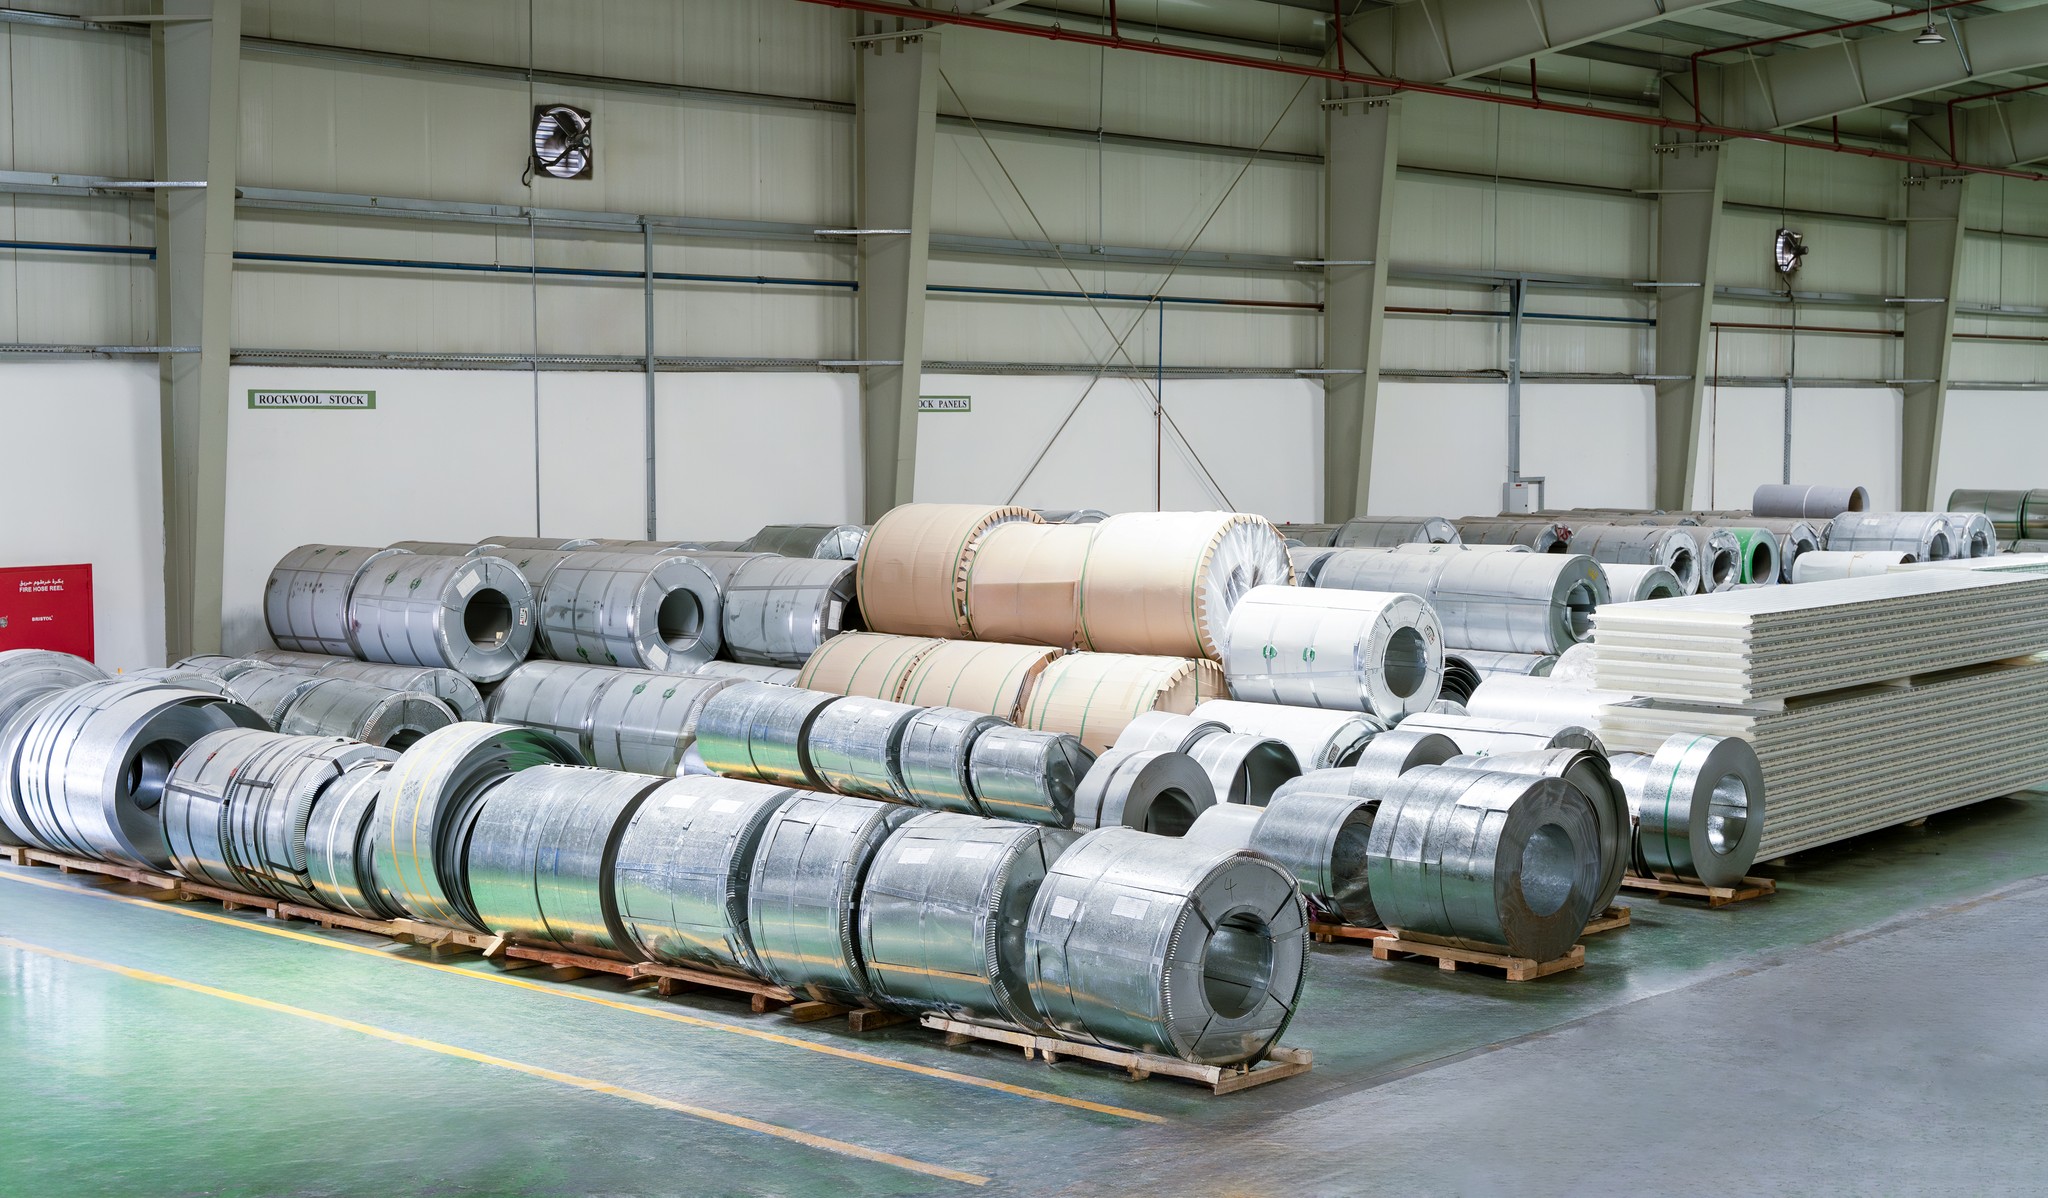
Our competitive advantage rests on raw material security and high-speed cold-roll fabrication capacity. We maintain substantial strategic inventories of prime structural steel coils sourced directly from globally qualified primary mills. Equipped with computerized fly-shearing and multi-axis hydraulic punch tooling, our roll-forming lines handle orders exceeding several thousand metric tons with consistent millimeter tolerances and expedited delivery cycles.

Enterprise Delivery Capabilities

  • Rapid Overland Dispatch Across the GCCDaily truck convoys to Riyadh, Dammam, Dubai, Abu Dhabi, Doha, and Manama with zero intra-GCC tariff obstacles.
  • Maritime Gateway via Sohar & SalalahFast containerized and breakbulk vessel dispatch serving East African ports (Mombasa, Dar es Salaam, Djibouti) without regional transit delays.
  • Full In-House QA/QC LaboratoryEvery production coil is rigorously tested for yield tension, elongation, zinc adhesion, and bend radius before fabrication.
  • Complete Envelope SynergyWe engineer purlins directly to support our PIR roof panels, profile sheets, and metal decking for single-source structural accountability.
Procurement Knowledge Base

Frequently Asked Questions on Cold Rolled Z Purlins

Clear, technically sound responses to the critical questions structural engineers, PEB fabricators, and commercial procurement directors ask when specifying cold-formed secondary steel.

Get a Quote

Cold rolled Z purlins possess asymmetric flanges (e.g., a top flange of 64 mm and a bottom flange of 58 mm) that permit identical profiles to nest inside each other at interior rafter supports. By lapping them across structural frames (typically 10% to 15% of the span), the system behaves as a continuous structural beam. This eliminates peak mid-span bending moments, drastically reduces deflection, doubles the structural section modulus over high-stress support zones, and achieves up to 25% to 35% steel weight savings compared to single-span framing.

For heavy industrial, coastal, or severe desert climates like the Arabian Gulf and coastal Africa, high-tensile structural grades conforming to BS EN 10346 (S350GD, S390GD, or S450GD) or ASTM A653M Grade 50/80 (minimum yield strength 350 to 550 MPa) are specified. For corrosion resistance, hot-dip galvanized coatings of Z275 (275 g/m² total both sides) or Galvalume (AZ150) are mandatory baseline standards. In harsh marine atmospheres within 3 km of the sea, Zinc-Aluminum-Magnesium (ZAM/Magnelis) coatings provide superior cut-edge self-healing protection.

The structural design rule-of-thumb for continuous Z purlin systems establishes a lap length between 10% and 15% of the total bay span centered over the portal frame rafter. For an 8-meter bay, a typical structural lap is 800 mm to 1,200 mm (400 mm to 600 mm on either side of the rafter centerline). In heavy snow, dynamic wind uplift, or high seismic zones, structural calculations may require double-span laps or staggered bridging to reinforce negative moment resistance.

Yes. Our computer-controlled roll-forming lines feature integrated automated hydraulic inline punch presses capable of executing complex web and flange hole patterns directly from Tekla or Revit BIM models. This includes round holes (14 mm, 16 mm, 18 mm), elongated slotted holes for thermal movement and erection tolerance (14x22 mm, 18x26 mm), and multi-tier sag rod / anti-sag bridging holes with sub-millimeter positional tolerance.

Manufacturing in Muscat, Oman provides strategic logistics advantages: zero customs duties across GCC member states (UAE, Saudi Arabia, Qatar, Kuwait, Bahrain), direct overland trucking transit within 24 to 72 hours, and rapid maritime container dispatch to East and North African ports via Sohar and Salalah ports without traversing congested regional choke points. This eliminates the 8 to 12 week transit risks inherent in sourcing from East Asia or Europe.

Every production batch from Emaar Industries is supplied with full Mill Test Certificates (EN 10204 Type 3.1) detailing chemical composition, yield strength, ultimate tensile strength, elongation, and zinc coating thickness verification. Finished purlins undergo dimensional tolerance checks according to BS EN 10162 and ASTM A653, backed by ISO 9001:2015 quality management oversight.

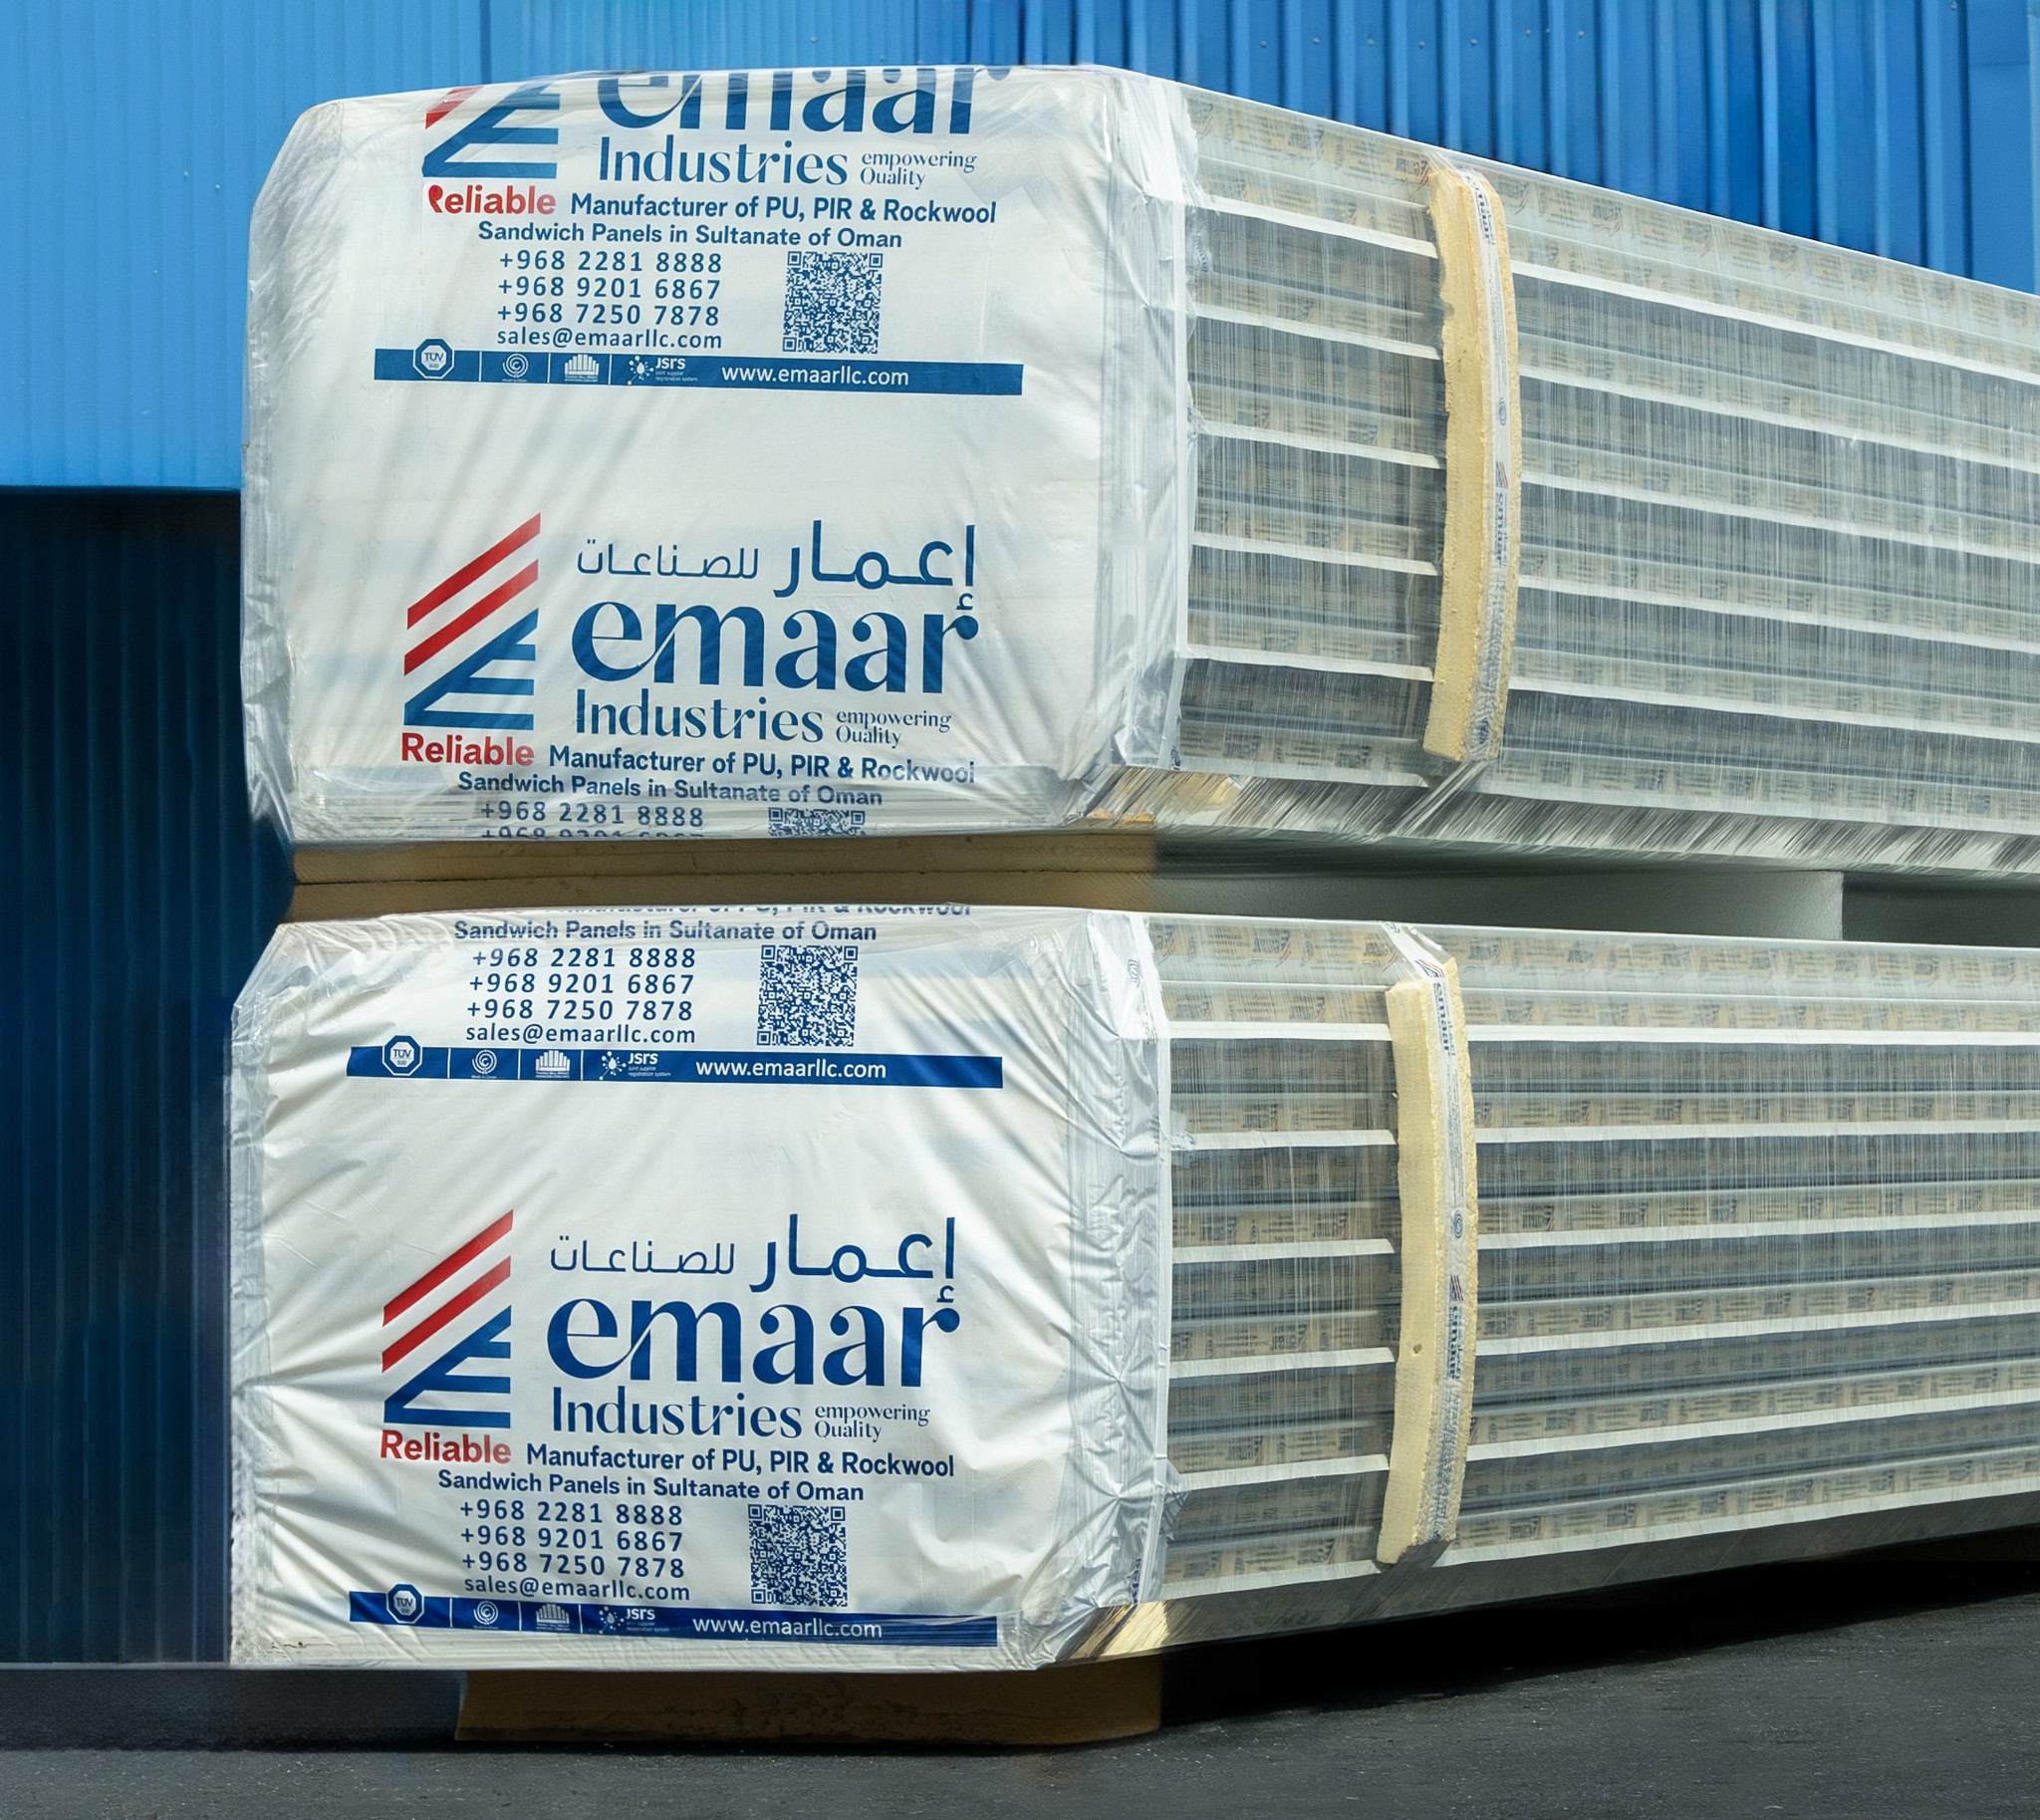
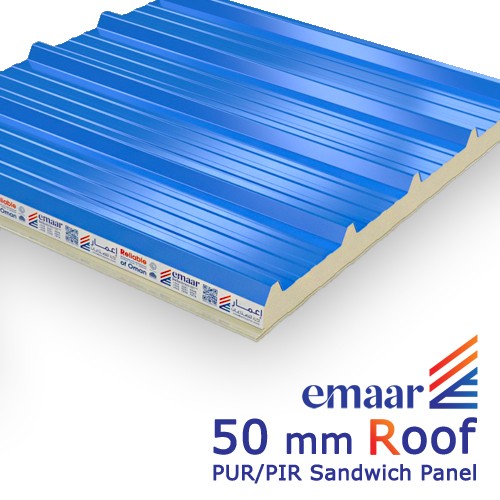
Because Emaar Industries manufactures PIR/PUR/Rockwool roof sandwich panels, profile sheets, and metal decking in parallel with cold-formed purlins, our structural engineers deliver a co-engineered envelope package. We provide matched fastener layouts, purlin flange widths tailored to panel crest frequencies, and thermal break isolators, eliminating on-site interface conflicts and structural submittal disputes.

Quality Certifications & Approvals

Engineered to International Structural Building Standards

Our cold-forming manufacturing lines, structural steel grades, and hot-dip galvanization processes comply strictly with ISO 9001:2015, BS EN 10346, BS EN 10162, and ASTM A653/A653M specifications. We supply pre-qualified engineering submittal dossiers to consultants, municipal authorities, and civil defence agencies throughout the GCC.

Download Quality Dossiers
Emaar Industries ISO and product certification marks
GCC & Export Reach

Direct Structural Engineering & Supply Hubs

Connect directly with our dedicated technical sales engineers for immediate design assistance, continuous lap span calculations, and competitive project quotations.