
Direct factory configurations manufactured to ASTM A653, EN 10346, and AS/NZS 4600 codes for continuous purlin runs, heavy solar payloads, and coastal framing integrity.
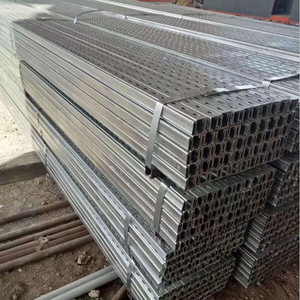
High-precision roll-formed slotted channel purlins designed for rapid module clamping and solar bracket arrays under extreme wind-shear environments.
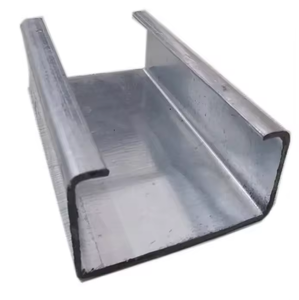
Hot-dip zinc coated C channels providing high yield rigidity across broad industrial spans, pre-engineered for direct rafter assembly with zero site-cutting.
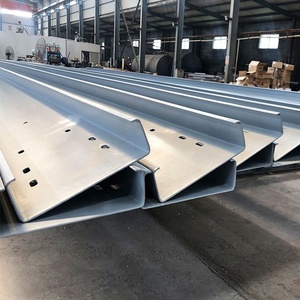
Pre-punched modular cold-formed sections offering automated bolting cleat configurations, suited for mezzanine secondary beams and complex roof column frames.
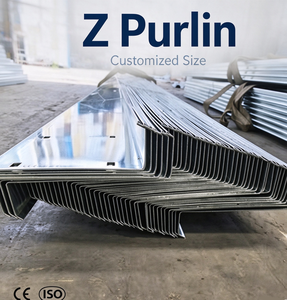
Engineered with nested asymmetrical flanges allowing continuous structural laps across multiple portal spans, maximizing bending moment resistance and reducing steel weight.
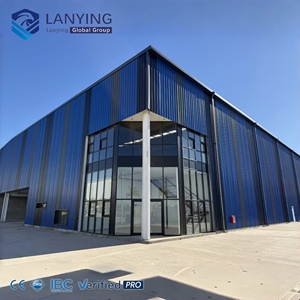
Complete secondary envelope package pairing heavy primary H-beams with cold-formed galvanised purlins and thermal sandwich cladding profiles.
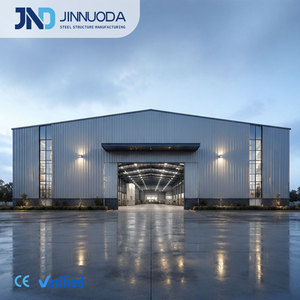
CE-approved structural members designed with reinforced return lips to counteract torsional flexure and lateral torsional buckling in high-snow-load regions.
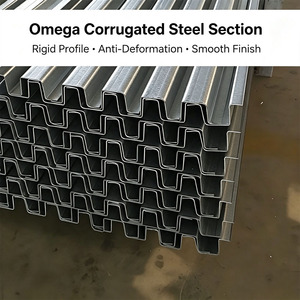
Specialized wide-flange hat-channel purlins developed for agricultural greenhouses, PV roof distribution decks, and light-gauge bridge ceiling spans.
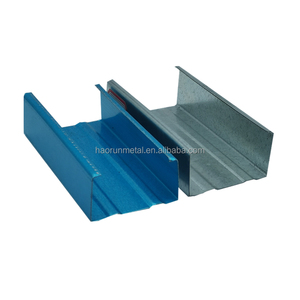
Calibrated specifically for international containerized shipping, featuring tightly regulated roll-forming tolerances, swaged ends, and protective bundling.
Selecting an overseas manufacturer requires evaluating more than cost-per-metric-ton. Structural reliability hinges on metallurgical purity, section modulus consistency, and precise environmental metallurgy.
Qualified exporters must certify cold-rolled coil inputs ranging from Q235B up to high-tensile G550/S550GD grades. The ratio between ultimate tensile strength (Rm) and yield strength (Re) determines seismic resilience and buckling survival under concentrated live loads.
Continuous hot-dip zinc coatings (Z120 to Z275) or Zinc-Aluminium-Magnesium (Zn-Al-Mg) alloys must endure tight-radius roll forming without micro-cracking at the outer bend radiuses. Flaking exposed at the lip or web compromises ASTM B117 salt-spray ratings.
Automated multi-stand roll-forming lines guarantee precision within ±1.0mm in web depth, flange angles, and lip dimensions. Minimizing sweep and camber along 12-meter continuous sections eliminates installation friction and racking across portal rafters.
| Profile Designation | Common Depths (mm) | Flange Widths (mm) | Thickness Range | Yield Strength (fy) | Optimal Structural Use |
|---|---|---|---|---|---|
| C-Purlin (Standard CEE) | 100 – 350 mm | 50 – 100 mm | 1.5 – 3.2 mm | 350 – 450 MPa | Single-bay spans, eave struts, door headers, wall girts |
| Z-Purlin (Symmetrical/Nested) | 120 – 300 mm | 50 – 75 mm | 1.5 – 3.0 mm | 450 – 550 MPa | Continuous multi-span portal frame roofing, lapped assemblies |
| Omega / Top Hat | 40 – 120 mm | 30 – 60 mm | 0.8 – 2.0 mm | 300 – 550 MPa | Solar PV fixing purlins, ceiling liner supports, light sheds |
| High-Strength Solar Rail | 60 – 150 mm | 40 – 60 mm | 1.8 – 2.5 mm | 400 – 550 MPa | Corrosive roof PV farms, heavy snow regions, ground arrays |
Global supply chain pressures and building envelope performance standards are shifting how developers, general contractors, and PEB manufacturers source secondary framing.
Heavy industry is migrating from traditional Z275 hot-dip galvanizing toward Zinc-Aluminum-Magnesium (e.g., ZM310) alloys. The presence of magnesium allows cut-edge self-healing protection, extending purlin structural lifespan in coastal industrial corridors up to 3 times longer without post-dipping cost.
Material inflation drives the adoption of thin-walled, high-tensile steel. Utilizing 550 MPa yield cold-rolled steel permits designers to down-gauge profiles from 2.5mm to 1.8mm while maintaining deflection thresholds, yielding up to 22% freight savings on trans-oceanic logistics.
Modern steel procurement demands exporter-side CNC file processing. Purlins arrive pre-punched with elongated slots, service knockouts, and match-stamped part numbers directly linked to Tekla Structures models, slashing site installation labor by up to 35%.
Modern cold roll-forming lines leverage continuous sensor diagnostics, high-speed flying shears, and servo-controlled punching tables to eliminate manufacturing stress cracks.
Automated quick-change tooling allows production facilities to transition from C150 to C300 or toggle between C and Z geometries in under ten minutes. This flexibility shortens mixed-order lead times for overseas export deliveries.
Cold-forming profiles with intermediate longitudinal web and flange stiffeners improves local buckling limits. These ribbed profiles allow purlins to support heavier composite insulation sheets and solar assemblies across spans of 8 to 12 meters.
International environmental ratings (LEED v4, BREEAM) increasingly require Environmental Product Declarations (EPD). Exporters operating Electric Arc Furnaces (EAF) with recycled steel scrap are displacing primary blast furnace suppliers across European and Middle Eastern projects.
Direct from our manufacturing base in Muscat, Oman, we supply complete cold-rolled structural packages and insulated envelope assemblies across the GCC, Africa, and global export destinations.
High-speed continuous roll-forming lines and advanced profiling mills produce up to 10,000 m² daily, ensuring reliable lead times for fast-track project phases.
More than 550 industrial facilities, distribution centers, hangars, and agricultural complexes rely on our secondary framing and insulated panel systems.
Every profile and coating system is calibrated to endure desert UV radiation, saline air, and summer temperatures exceeding 45°C without premature degradation.
Logistics reach across Oman, the UAE, Saudi Arabia, Qatar, Bahrain, Kuwait, and African corridors, backed by regional technical teams for site coordination.
We eliminate supply friction by manufacturing both cold-rolled structural purlins (C, Z, and Omega sections) and insulated building panels (PIR, PUR, Rockwool, decking, and architectural flashings) under one quality management system. This ensures seamless fit-up, coordinated delivery sequencing, and unified submittal documentation.
Answers to essential questions covering structural deflection limits, galvanization standards, and overseas packing specifications.
Send your structural framing schedules, required purlin spans, and delivery destination. Our engineering team will review your specifications and provide certified loading models within 24 hours.
Our sales engineers respond to project questions during working hours (GST+4).