
To achieve structural equilibrium, cold-formed galvanized Z purlins work in unison with high-density composite wall panels, specialized roofing profiles, cold-chain thermal envelopes, and airtight flashing assemblies. Explore our precision-manufactured product portfolio below.
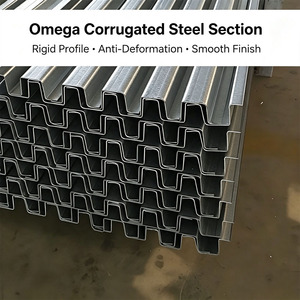
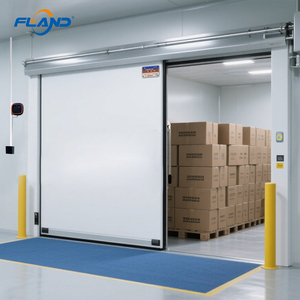
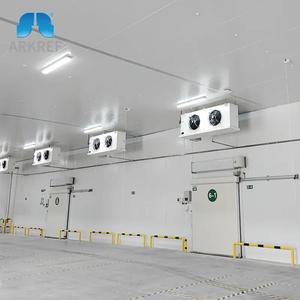
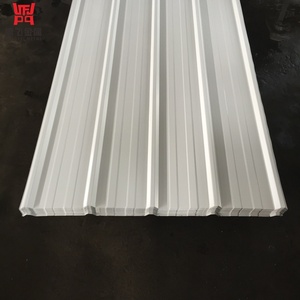
In contemporary Pre-Engineered Steel Buildings (PEB), industrial mega-warehouses, and heavy commercial envelopes, the selection of secondary structural framing directly governs total structural weight, roof stability, and erection economics. Galvanized Z Purlins (Z-sections) represent a monumental leap over traditional hot-rolled channel sections, delivering an exceptional strength-to-weight ratio achieved through precision computer-controlled cold roll-forming of high-tensile structural coil.
Unlike symmetrical C-sections, the principal axes of a cold-formed Z purlin are oriented diagonally to the web plane. When installed on pitched roof rafters, the asymmetric geometry allows the purlin to bend around its major principal axis under gravity loads, countering the lateral torsional buckling typical in sloped applications. More crucially, our automated manufacturing process creates unequal flange widths (for instance, a 62 mm top flange paired with a 68 mm bottom flange). This geometric differential permits seamless nesting and overlapping of adjacent purlins over interior structural column lines. The continuous lap creates a moment-resisting double-thickness structural continuity across critical support regions, effectively slashing positive mid-span bending moments by up to 40% and allowing engineers to specify thinner baseline gauges while achieving superior span-to-deflection ratios.
| Profile System | Structural Configuration | Lap Continuity Capability | Steel Weight Savings | Optimum Span Range | Primary Global Standard |
|---|---|---|---|---|---|
| Galvanized Z Purlin | Cold-Formed Continuous Nested | Full Moment Lap (10–15% L) | 30% – 42% vs Hot-Rolled | 6.0 m – 12.0 m Spans | EN 1993-1-3 / AISI S100 |
| Galvanized C Purlin | Cold-Formed Simply Supported / Sleeved | Requires Sleeve Bracket Joiners | 20% – 28% vs Hot-Rolled | 4.5 m – 7.5 m Spans | ASTM A653 / AS/NZS 4600 |
| Hot-Rolled PFC / U-Beam | Heavy Gauge Solid Flange | Non-Overlapping Butt Connection | Baseline Reference (0% Savings) | 5.0 m – 9.0 m (Heavy Dead Load) | GB/T 700 / ASTM A36 |
| Omega / Top-Hat Purlin | Cold-Formed Multi-Flange Stiffened | Continuous Direct Fastening | 15% – 25% Savings | 3.0 m – 6.0 m (Solar / Agro Sheds) | EN 10346 / DIN 59413 |
As China's leading manufacturing authority, our production lines utilize mill-certified hot-dip galvanized steel strip conforming to S350GD+Z275, S450GD+Z450, and ASTM A653 Structural Steel Grade 50/55. With precision automated online punch presses, every purlin receives custom-dimensioned elongated holes, eave-strut slots, and anti-sag bridging perforations executed prior to roll-forming. This completely eliminates cold-work micro-cracking and maintains uncompromised zinc coating integrity across fastener entry zones.
Selecting the appropriate surface passivation and coating mass is critical to preserving structural integrity in aggressive environments, from Middle Eastern coastal humidity to heavy chemical exposure.
Designed for dry inland warehouses, light manufacturing workshops, and climate-controlled commercial buildings. Features 20–25 µm total zinc coating thickness, delivering exceptional ductility during roll-forming with zero flake or micro-fissure separation.
Engineered for high-humidity coastal zones (ISO 12944 C4/C5 classification), port logistics hubs, and offshore cargo centers. Heavy zinc barrier mass prevents red rust initiation for 25+ years without demanding post-installation wet protective painting.
Zinc-Aluminum-Magnesium (Zn-Al-Mg) specialized ternary alloys. Delivers self-healing corrosion resistance along raw sheared edges and CNC-punched bolt holes through dense basic zinc hydroxide-magnesium carbonate protective film precipitation.
Tekla Structures and Revit 3D model exports integrate directly into high-speed cold roll-forming controllers via DSTV/NC1 protocols. Eliminates manual detailing oversights, ensuring zero-error alignment across thousands of variable pitch holes.
Shift toward S450GD and S550GD ultra-high tensile yield steels. Combined with stiffened edge lips and intermediate flange web indentations, this enables up to 22% secondary structural weight reduction, lowering shipping volumes and crane hoisting time.
New warehouse specifications demand purlin systems engineered for retrospective Commercial & Industrial (C&I) photovoltaic retrofits. Pre-punched dual-web attachments allow clamp systems to mount directly without drilling into protected galvanized envelopes.
Global EPC procurement protocols mandate audited Environmental Product Declarations (EPD) and CBAM carbon footprint verification. Our coils are increasingly sourced from scrap-fed Electric Arc Furnaces (EAF) with 60% lower embedded carbon dioxide intensity.
Drawing from extensive reference project deliveries across the GCC, Africa, and Central Asia, we combine heavy manufacturing throughput with rigorous metallurgical quality systems.
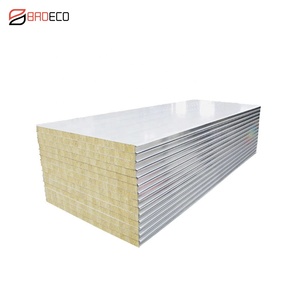
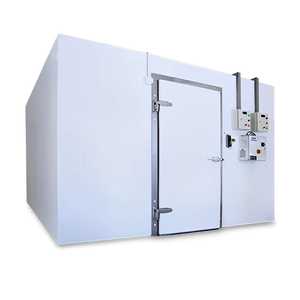
We are not merely a cold-roll shop; we engineer and supply the full external envelope. From cold-formed Z and C secondary framing to Class A1 mineral Rockwool wall panels, PIR/PUR roof systems, cold store insulated doors, and color-matched flashing profiles, you receive a dimensionally synchronized building envelope from one single source.
Every parent coil batch undergoes rigorous verification: mechanical tensile tests (Yield, Tensile Strength Rm, Elongation A80), zinc weight X-ray fluorescence audits, magnetic coating thickness verification, and copper-accelerated acetic acid salt spray tests (CASS) adhering strictly to EN 10204 Type 3.1 certification frameworks.
Z-purlins naturally compact together for dense nesting. Our automated bundling units strap nested profiles with protective heavy timber dunnage, anti-chafing polymer wraps, and lifting lug bridles. This prevents transit de-galvanization and ensures maximum tonnage packing inside standard 40ft High Cube containers.
The primary failure mode in cold-formed roof systems is not pure shear, but rather combined bending and web crippling at support rafters, or excessive downward sag prior to cladding screw engagement. When designing a continuous nested Z purlin run, engineers must calculate the lap length based on structural span ($L$). As a proven empirical rule of thumb validated by finite element simulations:
Maintain an overlap length between 0.10L and 0.15L (e.g., for an 8.0 m structural bay, the lap should measure 800 mm to 1200 mm centered over the rafter flange). This positions the lap endpoints close to the inflection point (zero moment) under uniform gravity loads.
For spans exceeding 6.0 m, install high-tensile threaded sag rods at mid-span or third-points. Sag rods tie top and bottom flanges together, preventing lateral twist during high suction wind reversal and providing working stability during panel laying.
Always utilize minimum Grade 8.8 hot-dip galvanized structural bolts with hardened washers through the pre-punched web holes into structural rafter cleats. Avoid field gas-cutting or torch reaming of holes, which burns away protective zinc barriers.
Authoritative answers to critical technical and logistical questions faced by structural consultants, estimators, and project directors.
Z-purlins offer two decisive structural advantages for roof framing: First, the orientation of their principal axes aligns more favorably with the roof pitch under downward gravity loads, helping prevent lateral deflection along the slope. Second, and most importantly, unequal flange widths allow Z purlins of the same depth to nest together directly over interior rafter supports. This nested lap acts as a double-thickness continuous beam connection that effectively redistributes negative bending moments across interior supports. C-purlins, by contrast, cannot nest without dedicated separate joint sleeves, which increases fastener counts, erection time, and baseline steel weight.
We manufacture Z purlins across a wide array of international structural standards. Base metal grades include ASTM A653 / A1063 Structural Steel Grade 50 (345 MPa minimum yield strength) or Grade 55 (380 MPa), as well as European standard EN 10346 S350GD, S390GD, S450GD, and S550GD. For corrosion protection, we supply hot-dip galvanized coatings spanning Z120 (120 g/m² combined both faces) up to ultra-heavy Z600 (600 g/m²). We also supply state-of-the-art Zinc-Aluminum-Magnesium (ZAM / SuperDyma / PosMAC) alloy coatings for corrosive coastal or heavy industrial environments.
Yes. Our computerized roll-forming lines feature multi-head, servo-driven hydraulic punch stations located before the initial profiling rolls. We can punch standard 14mm, 18mm, or 22mm round bolt holes, elongated slotted holes (such as 18x26mm or 22x30mm) for thermal expansion allowance, as well as specialized sag rod holes located directly in the web or flange stiffeners according to your structural engineering drawings or Tekla NC1 export data.
Because Z purlins nest closely, inter-profile friction during maritime transport can cause superficial rub marks. We apply a light passivation seal or dry organic lubricating film to the galvanized strip. Automated bundlers bundle profiles into tight, solid blocks using heavy PET strapping over corner protection guards. Heavy timber dunnage keeps packs elevated above container floors, ensuring bundles arrive clean and ready for direct crane hoisting.
Our automated profiling equipment operates under tight dimensional tolerances governed by BS EN 10162 and AISI S100. Typical manufacturing tolerances are: Web depth ($H$) ±1.0 mm; Flange widths ($B_1$, $B_2$) ±1.0 mm; Flange lip stiffener ($C$) ±1.5 mm; Total cut length ±2.0 mm; Camber and bow less than $L/1000$. This dimensional precision guarantees smooth on-site nesting without binding or forced hydraulic clamping.
To provide an accurate technical and commercial proposal, our engineering estimation desk requires: (1) Purlin profile designation or dimensions (Web depth $H$, Flanges $B_1/B_2$, Lip $C$, and thickness $t$ in mm); (2) Steel grade and minimum yield strength requirement; (3) Desired zinc coating weight (e.g., Z275, Z350, Z600); (4) Frame span spacing and purlin lap length; (5) Hole punching schedule or Tekla model file; and (6) Total linear meters or project tonnage with target port of delivery.
Contact our senior structural estimating team today for mill test certifications, custom Tekla detailing support, or factory-direct pricing on Galvanized Z Purlins, continuous framing systems, and complete building envelopes.
Our sales engineers respond to project questions during working hours (GST+4).