
Manufactured under strict ISO 9001 and international standards, our structural purlins and high-performance cladding systems provide complete thermal, structural, and moisture-tight performance for Greater Ho Chi Minh City industrial assets.
A comprehensive examination of cold-formed asymmetric Z-sections under biaxial bending, negative moment lap redistribution, and torsional restrain systems.
By nesting sections over intermediate portal frames, our Z-purlins double the section modulus ($Z_x$) at peak stress zones, converting independent beam flexure into an efficient continuous multi-span load path.
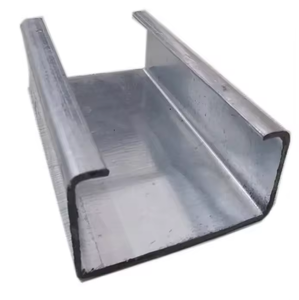
Our computerized roll-forming tooling rolls edge stiffener lips at calculated angles (45° to 55°), maximizing the rotational spring stiffness ($K_{\phi}$) and suppressing torsional-flexural buckling modes under cyclonic wind uplift.
Continuous framing slashes live-load roof deflection down to $L/250$ or $L/300$, preventing micro-cracking in exterior PIR panels, joint disengagement, and ponding water accumulation during peak monsoon downpours.
Optimizing purlin coatings, zinc alloy compositions, and structural thermal performance for the humid tropical climate of the Dong Nai and Saigon River basins.
E-commerce fulfillment centers require expansive column grids (up to 9m or 10m bay spacings). Our cold-rolled Z250 and Z300 sections support multi-bay continuity, minimizing steel column density and maximizing automated storage retrieval headroom.
Cold storage facilities using high-density polyurethane and PIR sandwich panels demand uncompromising structural stability. Thermal cycling between indoor -25°C freezers and +38°C outdoor ambient temperatures requires precision pre-punched slotted holes to accommodate thermal creep.
Electronics and precision component fabrication plants mandate zero roof leakage risk and non-combustible building envelopes. Our Z-purlins integrate seamlessly with Class A rockwool roof systems and continuous galvanized metal roof decking.
Precision cross-sectional data for structural consultants, steel fabricators, and PEB engineering teams operating in Vietnam.
| Profile Code | Web Depth (D) mm | Flange Top/Bottom mm | Stiffener Lip mm | Thickness (t) mm | Steel Grade & Yield ($f_y$) | Mass (kg/m) | Moment of Inertia ($I_x$ cm⁴) |
|---|---|---|---|---|---|---|---|
| Z150-18 | 150 | 62 / 56 | 18 | 1.8 | Q355 / G450 (450 MPa) | 4.12 | 142.6 |
| Z180-20 | 180 | 68 / 62 | 20 | 2.0 | G450 / G550 (550 MPa) | 5.34 | 248.9 |
| Z200-20 | 200 | 72 / 65 | 20 | 2.0 | G450 / G550 (550 MPa) | 5.78 | 332.1 |
| Z200-25 | 200 | 72 / 65 | 22 | 2.5 | G450 / G550 (550 MPa) | 7.18 | 408.4 |
| Z250-25 | 250 | 78 / 70 | 22 | 2.5 | G450 / G550 (550 MPa) | 8.32 | 745.2 |
| Z300-30 | 300 | 85 / 75 | 25 | 3.0 | G450 / G550 (550 MPa) | 11.45 | 1,420.5 |
Note: Custom dimensions, asymmetrical flange sizing for nesting clearances, and custom CNC punch hole patterns (standard gauge lines: 14x22mm slotted or round) are manufactured to project shop drawings.
Evaluating load-to-weight efficiency, procurement economics, and installation speed for commercial procurement directors.
| Evaluation Factor | Continuous Cold-Rolled Z-Purlin | Simple-Span Cold-Rolled C-Purlin | Traditional Hot-Rolled U/Channel |
|---|---|---|---|
| Structural Continuity | Continuous over multiple bays via 180° nested lap joints | Discontinuous (Simple Span); requires complex bracket splice plates | Discontinuous; bolted or welded directly to rafter brackets |
| Steel Consumption | Base Index (100%) - Optimal strength-to-weight ratio | 125% - 135% heavier due to unassisted mid-span moment peaks | 160% - 210% heavier; high dead load increases frame sizing |
| Deflection Performance | Up to 50% lower deflection ($L/250$ to $L/300$ easily met) | Higher mid-span deflection; limited to shorter bay lengths (<6m) | Rigid, but heavy self-weight contributes to dead-load sag |
| Corrosion Protection | Mill-applied continuous hot-dip galvanized (Z275 / AZ150) | Mill-applied continuous hot-dip galvanized (Z275 / AZ150) | Requires post-fabrication shot blasting & manual painting/galvanizing |
| Site Assembly Velocity | Factory pre-punched holes; rapid overlapping; zero on-site welding | Pre-punched; requires butt-joint brackets and double cleat fasteners | Slow; field drilling, heavy craning required, frequent touch-up painting |
How green building standards, rooftop photovoltaic integration, and automated manufacturing are driving changes in structural specifications.
Under Vietnam’s Power Development Plan 8 (PDP8), industrial rooftop solar is mandatory for multinational exporters. Retrofitting solar arrays imposes additional dead loads of 15–22 kg/m² plus localized wind vortex uplifts. Specifying continuous Z-purlins with G500 high-yield steel accommodates this additional structural capacity without requiring rafter strengthening.
Industrial parks are transitioning to green facility certifications. Cold-rolled Z-purlins contribute substantially to Materials and Resources (MR) credits through high post-consumer recycled steel scrap content, reduced structural tonnage, 100% recyclability, and reduced transport emissions through optimized nested bundling.
Modern structural steel detailing in Southern Vietnam utilizes Tekla Structures and Revit software. Our automated roll-forming lines ingest direct DSTV/CAM data, executing web and flange punches with ±1.0 mm accuracy, eliminating site reaming and accelerating installation schedules.
Combining world-class production infrastructure, full metallurgical batch traceability, and rapid ocean container logistics to Cat Lai and Cai Mep ports.
With an automated production capacity exceeding 10,000 m² of panels and hundreds of metric tons of cold-formed structural sections daily, we guarantee delivery schedules for large-scale industrial projects.
Every coil batch is delivered with EN 10204 3.1 inspection certification, documenting chemical analysis, yield stress ($f_y$), tensile strength ($f_u$), elongation percentage, and zinc mass verification.
Advanced German and Taiwanese multi-station roll-forming lines apply progressive roller passes, preventing micro-stress fractures along bend radii and maintaining accurate cross-sectional geometry.
Asymmetric Z-purlins nest tightly together, dramatically maximizing sea container shipping payloads into Cat Lai Port and slashing ocean freight costs per ton compared to bulk structural shapes.
Essential guidance for project developers, EPC general contractors, and structural consultants procuring cold-formed sections for Southern Vietnam.
Continuous Z-purlins nest over intermediate frames to double the section modulus at support points. This redistributes bending moments and reduces mid-span deflection by up to 50% compared to simply-supported C-sections. This allows longer bay spans (7.5m to 9m) and reduces secondary structural steel weight by up to 35%.
For standard inland facilities (VSIP Binh Duong), a hot-dip galvanized coating of Z275 (275 g/m² total both sides) is standard. For installations within 20km of the coastal waterways, mangrove river basins, or chemical logistics clusters (Nhon Trach, Cat Lai, Phu My), we recommend Z350 or 55% Aluminium-Zinc alloy (AZ150 Galvalume) to prevent early corrosion from salt spray and industrial emissions.
In accordance with AS/NZS 4600 and AISI S100 specifications, optimal lap length typically ranges between 10% and 15% of the center-to-center span between portal frames. For example, an 8.0-meter bay spacing requires a total nested lap of 800mm to 1200mm (centered directly over the structural rafter), secured with structural bolts through web pre-punched holes.
Yes. By utilizing high-yield G450 or G550 steel substrates (yield strength 450 to 550 MPa), our continuous Z-purlins can be engineered to support additional dead loads (15-20 kg/m² for solar panels, racking, and inverters) plus dynamic wind uplift without exceeding deflection criteria ($L/200$ total load).
Our production lines feature automated inline hydraulic punching systems capable of punching standard web slots (typically 14mm x 22mm for M12 structural bolts) and round flange holes based on project shop drawings. This pre-punching ensures alignment across lap joints and eliminates field torch-cutting or drilling.
When fastening zinc-aluminium coated roof sheets or sandwich panels to galvanized Z-purlins, we recommend Class 3 or Class 4 mechanical fasteners (AS 3566.2) equipped with bonded EPDM washers. For corrosive applications, isolation barrier tape is applied across purlin top flanges to avoid direct contact between dissimilar metals.
Every shipment is accompanied by Mill Test Certificates (MTC) conforming to EN 10204 Type 3.1, certifying mechanical yield, ultimate tensile strength, elongation, and coating mass verification. In addition, factory ISO 9001, ISO 14001, and third-party laboratory tensile/corrosion test reports are provided for consultant submittal packages.
Due to their asymmetric design, Z-purlins nest tightly together in compact, strapped bundles with corner edge protectors and moisture-barrier plastic wrapping. This maximizes container cube utilization (up to 26–28 metric tons per 40ft high-cube container) and prevents transit abrasion and moisture accumulation during ocean freight into Cat Lai Port.
Consult with our technical sales engineers for structural optimization, custom purlin calculations, lap joint schedules, and competitive factory-direct pricing for your upcoming industrial project.
Inquire NowOur sales engineers respond to project questions during working hours (GST+4).