
Structural Secondary Framing & PEB Substructures

China Top Steel Substructure Purlins Manufacturers & Exporters

High-Yield Cold-Formed C/Z/Sigma Galvanized Purlin Systems, Continuous Lapped Substructures, and Integrated Building Envelope Solutions Engineered for Global Pre-Engineered Steel Projects.

Precision Structural Components

Engineered Substructures & Envelope Product Series

Manufactured with continuous CNC roll-forming lines, automated punching units, and strict EN 1090/ASTM certifications, our product matrix bridges secondary steel structural purlins with high-performance building envelope systems.
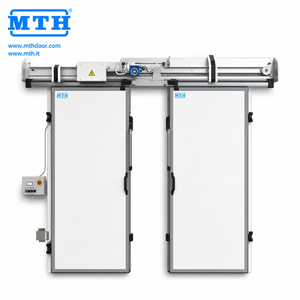
Airtight System Custom Size Thermal Insulation Color Steel Plate Motorized Double Open Airtight Commercial Walk In Cooler Cold Room Sliding Door

Custom Size Thermal Insulation Color Steel Plate Motorized Double Open Airtight Cold Room Sliding Door

Engineered for temperature-controlled cold logistics hubs, featuring polyurethane insulation cores, heated perimeter perimeter seals, and heavy-duty structural steel headers designed for purlin integration.
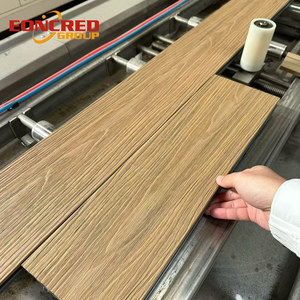
Composite Deck Robust Composite Decking Stable Outdoor Flooring,panel for Exterior Wall Panel

Robust Composite Decking Stable Outdoor Flooring,panel for Exterior Wall Panel

Engineered high-durability composite paneling engineered to withstand outdoor climate extremes, high pedestrian shear stresses, and direct mechanical fastening to steel substructure secondary girts.
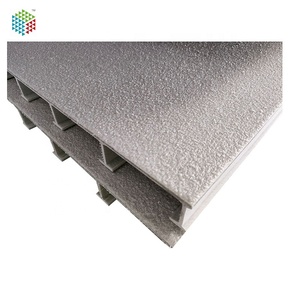
Heavy-Duty FRP Outdoor Structural FRP Deck Boards

Outdoor Structural FRP Deck Boards

Corrosion-proof fiberglass reinforced polymer decking systems with high strength-to-weight ratios, perfect for coastal industrial corridors, marine platforms, and chemical environment walkways.
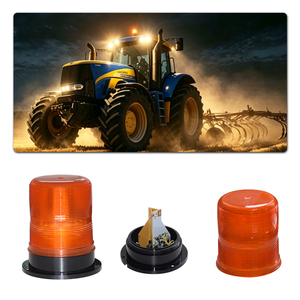
Safety Lighting New WTTG Automotive Flashing Signal Light with LED Strobe Lamp DC12V/24V IP65 Waterproof for Road Hazard Warning Car Roof Mount

New WTTG Automotive Flashing Signal Light with LED Strobe Lamp DC12V/24V IP65

Heavy-duty IP65 waterproof automotive safety strobe lighting engineered for logistics yard transport equipment, overhead maintenance cranes, and industrial site emergency vehicles.
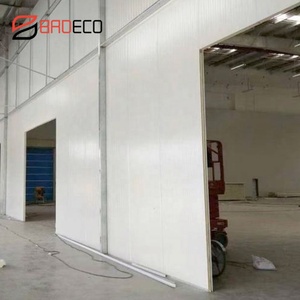
Insulated Partition Insulated Partition Single Slot Cold Storage Wall Sandwich Panels For Internal Division Of Warehouse

Insulated Partition Single Slot Cold Storage Wall Sandwich Panels

High-density internal division panels engineered for temperature zoning in industrial warehouses, offering seamless interlock tongue-and-groove joints that anchor securely to vertical steel purlin girts.
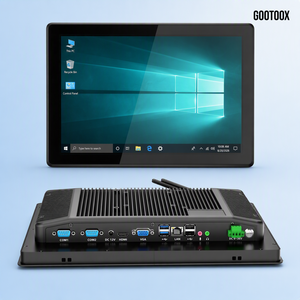
Industrial IoT Industrial Panel PC 12 Inch 13.3 Inch 15 Inch 15.6 Inch 21.5 Inch Embedded Fully Sealed Fanless Cold Chain Management Panel

Industrial Panel PC 12 to 21.5 Inch Embedded Fanless Cold Chain Management Panel

Fully sealed IP65 touchscreen industrial control PCs designed for harsh temperature-controlled facilities, enabling automated environmental monitoring, structural strain tracking, and HVAC automation.
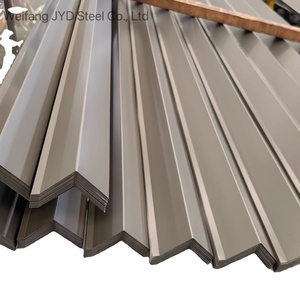
Roof Flashing Roofing Flashing 2x2/2.5x2/3x3inch Drip Edge Galvanized Steel Flashing Roof Edge Trim

Roofing Flashing Drip Edge Galvanized Steel Flashing Roof Edge Trim

Precision cold-formed galvanized and zinc-aluminum-magnesium edge trims, engineered to prevent water ingress along roof eaves while providing clean mechanical termination at purlin lines.
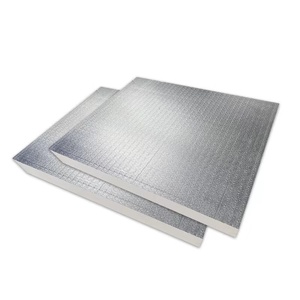
Thermal Core Easy Installation PF Insulated Panel Aluminum Foil Phenolic Foam Insulation Floor Board for Cold Room

Easy Installation PF Insulated Aluminum Foil Phenolic Foam Floor Board

Ultra-low thermal conductivity insulation floor boards clad with embossed aluminum foil, providing superior compressive resistance over structural decking in refrigerated warehouse facilities.

550+
Major Projects Delivered Worldwide
10,000 m²
Daily Integrated Envelope Capacity
550 MPa
Ultra-High Tensile Yield Option
Z275/ZM
Heavy Galvanized & Zn-Al-Mg Coatings
Engineering White Paper

Technical Superiority in Steel Substructure Purlin Engineering

Cold-formed thin-walled steel secondary structural members serve as the crucial backbone of pre-engineered steel buildings (PEB), industrial plants, and logistic centers. Understanding the structural behavior of C, Z, and Sigma purlins is critical for modern lean construction.

In modern industrial structural design, the substructure framing system represents roughly 25% to 35% of total structural steel tonnage, while carrying 100% of the external roof and wall loads—including wind suction, seismic forces, solar dead-loads, and snow drifts. As China's leading manufacturer and exporter of cold-formed secondary framing systems, we produce high-yield purlins configured specifically to eliminate localized web crippling and lateral-torsional buckling. By leveraging computerized continuous roll-forming lines with high-speed automated flying punches, our C-purlins and Z-purlins are fabricated with microscopic tolerances (±1.0 mm linear straightness), optimizing load distribution across portal frames and clear-span structures.

Structural Optimization Note: Z-purlins offer a decisive structural advantage over traditional hot-rolled channel sections or standard C-sections in multi-span roofing designs. Because Z-sections can be rotated and nested at support columns, structural engineers can achieve a continuous beam lap configuration. Continuous lapping over portal frame rafters reduces maximum mid-span bending moments from $M = \frac{wL^2}{8}$ (simply supported) down to approximately $M = \frac{wL^2}{12}$ at supports, permitting up to a 20% to 28% reduction in purlin steel mass while increasing deflection resistance under negative wind uplift.

Our raw material sourcing strictly enforces prime structural coil specifications. We utilize high-grade hot-dip galvanized steel conforming to ASTM A653 / A653M (Grades 50, 60, and 80), EN 10346 (S350GD, S450GD, and S550GD+Z), and GB/T 2518 (Q235B and Q355B). When exposed to coastal environments, high salinity, or aggressive chemical vapours (such as ammonia emissions in livestock sheds or chlorine in water treatment plants), our export division specializes in applying Zinc-Aluminum-Magnesium (Zn-Al-Mg / ZM) coatings. The presence of 1.5% to 3.0% magnesium in the eutectic alloy forms a crystalline simonkolleite barrier that automatically precipitates over sheared cut edges and punched bolt slots, offering self-healing corrosion resistance superior to traditional batch hot-dip galvanizing.

Profile Geometry Structural Profile Dynamics Steel Grade & Yield Strength Optimal Bay Spacing Primary Industrial Applications
C-Section Purlin Mono-symmetric channel with inward-stiffened lips; simplifies perimeter framing & wall girts. Q235B / S350GD (350 MPa) 4.0 m – 6.5 m Spans Wall cladding girts, door headers, eaves struts, window trimmers, parapet frames.
Z-Section Purlin Point-symmetric with nested unequal flanges (e.g., 65mm & 60mm) enabling continuous support lapping. Q355B / S450GD (450 MPa) 6.0 m – 10.5 m Spans Primary roof purlins for clear-span warehouses, distribution centers, aircraft hangars.
Sigma (Σ) Profile Web-stiffened profile providing superior cross-sectional moment of inertia against web crippling. S450GD / S550GD (550 MPa) 8.0 m – 12.0 m Spans Heavy-load mezzanines, high snow load regions, extended bay logistical centers.
Zinc-Al-Mg (ZM) Purlin Self-healing cut edge protection; triple corrosion lifespan in ISO 9223 C4/C5 environments. ZM275 - ZM310 Alloy Versatile Multi-Span Coastal port terminals, chemical processing factories, agro-industrial and cold-chain buildings.
Manufacturing Prowess

Why Engineering Contractors Rely on Our Manufacturing Base

From raw coil slitting to precision cold-roll-forming, in-line punching, and international container packaging, our vertically integrated plant in China delivers unmatched structural reliability.

Fully Automated CZ Quick-Change Lines

Equipped with PLC-driven quick-change roll-forming mills, transitioning between C and Z profiles (web heights 80mm to 400mm, thicknesses 1.5mm to 3.5mm) takes under 15 minutes. This agility ensures mill-run custom lengths without cutting waste.

Precision CNC Pre-Punching & Slotting

Custom bolt-hole patterns (round holes, slotted holes for thermal expansion, staggered lap configurations) are punched directly on-the-fly with 0.5mm positional accuracy, eliminating on-site flame cutting and drilling during PEB assembly.

Certified Metallurgical Quality Assurance

Every batch undergoes rigorous quality checks: 100% coil heat number tracking, spectral chemical composition analysis, tensile and 180° cold bend testing, and ultrasonic zinc coating thickness verification according to ISO 9001 and CE EN 1090 standards.

Turnkey Building Envelope Synergy

Beyond secondary framing, our facilities manufacture cold storage doors, PIR/Rockwool insulated sandwich panels, composite decking, and roof flashing trims, providing international EPCs with a unified single-source building envelope ecosystem.

Optimized Nested Container Packaging

Z-purlins and nested C-sections are tightly bundled using high-tensile steel strapping and custom wooden cradles with desiccant protection. This high-density nesting maximizes 40ft High Cube container payloads up to 26–28 metric tons, slashing shipping costs.

Global EPC Track Record & Technical Support

With over 550 projects supplied across the Middle East (GCC), Southeast Asia, Africa, Europe, and the Americas, our multi-lingual structural engineering department provides structural layout checks, Tekla detail verification, and prompt site submittals.

Market Intelligence & Forecast

Future Procurement Trends in Steel Substructures (2025–2030)

Global supply chains are shifting toward lean, low-carbon, and highly corrosion-resistant structural assemblies. Staying ahead of these procurement trends ensures competitive bidding and project longevity.

Material Evolution

Rapid Transition to Zinc-Aluminum-Magnesium

International contractors are actively phasing out standard Z275 hot-dip galvanizing in favour of Zinc-Aluminum-Magnesium (e.g., ZM310, SuperDyma, PosMAC). ZM provides up to 5 times the atmospheric corrosion protection in industrial zones while offering autogenous self-healing over sheared purlin ends, completely eliminating post-fabrication galvanizing dips.

Structural Efficiency

Adoption of S450GD & S550GD High-Yield Steels

Procurement engineers increasingly demand higher yield steel grades ($F_y \ge 450 \text{ MPa}$ to $550 \text{ MPa}$) rather than legacy Q235B ($235 \text{ MPa}$). By specifying higher tensile steels with optimized cross-sectional lip geometry, projects reduce steel consumption by 18% to 26%, dramatically cutting freight and crane erection costs.

Digital Integration

Direct BIM-to-Machine Integration (Tekla NC1)

Paper drawing handovers are vanishing. Modern procurement workflows now mandate direct transmission of digital 3D models (Tekla NC1 files) straight into our CNC cold-roll-forming lines. This automated data flow delivers zero-defect bolt alignment, automated marking, and grouped bundle sequencing directly matched to on-site erection phases.

Sustainability & ESG

Low-Carbon Steel & EPD Environmental Certification

With the implementation of the European Union's Carbon Border Adjustment Mechanism (CBAM) and North American green building mandates (LEED v4.1), steel substructure procurement requires verified Environmental Product Declarations (EPD). Our mills integrate EAF (Electric Arc Furnace) scrap feeds to offer verified low-carbon structural purlins.

Renewable Synergy

BIPV & Solar-Ready Dual-Purpose Purlins

Commercial warehouse roofs are universally required to accommodate rooftop photovoltaic arrays. Procurement trends demand secondary structural purlins pre-engineered with higher torsional stiffness and pre-punched mounting interfaces capable of supporting combined wind uplift, maintenance live-loads, and solar ballast weights.

Supply Chain Security

Consolidated Multi-Component Envelope Sourcing

Procurement leaders are abandoning fragmented procurement where purlins, insulated roof panels, composite floor decks, and drip flashings are bought from separate vendors. Consolidated single-source procurement eliminates interface mismatch disputes, simplifies LC financing, and optimizes container stowage.

Technological Frontiers

Advancements in Cold-Formed Substructure Manufacturing

Breakthroughs in metallurgical forming, high-frequency continuous annealing, and anti-torsional profile geometry are redefining structural secondary framing.

Precision Forming

Progressive Multi-Station Roll Pass Dynamics

Utilizing 18 to 24 progressive cold-forming roll stations prevents residual internal stress concentrations at corner bends, ensuring high-strength steels do not crack along sharp bend radii during extreme cold-weather service.

Anti-Buckling

Compound Flange Lip Stiffeners

Engineered with complex 45° returned lip returns and return-flange stiffeners, our high-span Z-sections provide up to 32% greater elastic local buckling resistance compared to primitive 90° single-lip profiles.

Smart Tracking

Laser Inkjet Part Identification & QR Tracking

Every individual purlin is marked on-the-fly with high-contrast laser inkjet printing indicating building grid location, profile dimension, steel grade, and heat number, accelerating on-site installation by over 30%.

Thermal Break

Acoustic & Thermal Isolation Bridging

Advanced factory-fitted thermal isolator clips and anti-capillary flange profiles reduce thermal bridging across the building envelope, meeting stringent modern building codes for conditioned and refrigerated facilities.

Procurement Guidelines

Technical Sourcing Checklist for International Buyers

To receive precise structural engineering calculations, mill pricing, and optimized container packing lists, make sure to specify these 8 primary parameters in your RFQ.

✓
1. Bay Spacing & Clear Spans
Center-to-center distance between main steel portal frames or structural trusses (typically 6m, 7.5m, 9m, or 12m).
✓
2. Steel Yield & Grade
Minimum specified yield point ($F_y$ = 235, 350, 450, or 550 MPa) required by structural design calculations.
✓
3. Environmental Exposure (C1-C5)
Site environmental corrosivity class (ISO 12944) to establish zinc mass ($Z120, Z275, ZM275, ZM310$).
✓
4. Dead, Live & Environmental Loads
Specific roof envelope dead weights, basic wind speed ($V_{ref}$), seismic factors, and local snow drift loads.
✓
5. Support Span Configuration
Specifying simply-supported single spans vs. continuous nested lap configurations (lapping ratio $0.10L$ to $0.15L$).
✓
6. Bolt Hole Geometry & Pattern
Round vs. slotted holes (e.g., $14\times22\text{mm}$ slots), web hole centers, and flange clearance for sag rods.
✓
7. Bridging & Sag Rod Integration
Requirements for round rod or angle sag struts to provide lateral restraint against torsional twisting.
✓
8. Destination Port & Packaging
Container discharge port restrictions, maximum bundle weight limitations for on-site mobile crane offloading.
Knowledge Base & Technical FAQ

Frequently Asked Questions by Structural Engineers & Buyers

Authoritative, engineering-backed answers addressing structural design standards, corrosion resistance, span calculations, and international shipping logistics.

Q1 What are the structural differences between C-purlins and Z-purlins?
C-purlins are mono-symmetric sections shaped like the letter 'C'. They are naturally self-standing and simple to bolt to side walls and openings, making them ideal for simple-span conditions, wall girts, and eaves framing. In contrast, Z-purlins are point-symmetric sections with unequal top and bottom flanges. This asymmetry allows one Z-purlin to rotate 180° and slide inside another over structural support beams. This continuous lapped connection produces continuity across multiple bays, significantly stiffening the entire roof against negative wind uplift and reducing total required steel thickness by 15% to 25%.
Q2 How is the optimal overlap lap length calculated for continuous Z-purlin systems?
According to standard cold-formed structural codes (such as AISI S100-16, Eurocode 3 EN 1993-1-3, and BS 5950-5), the recommended lap length over portal frames is typically between 10% and 15% of the clear bay span on each side of the rafter center line (yielding a total overlap length of $0.20L$ to $0.30L$). For example, on a 6.0-meter bay span, a total lap of 900mm to 1200mm centered over the rafter creates an effective structural hinge that evenly redistributes negative moment peaks across the support points.
Q3 What international steel standards and certifications do your purlins satisfy?
Our secondary steel structural purlins are fully certified to international standards:
  • American Standard: ASTM A653 / A653M (Grades 33, 40, 50, 60, 80) and ASTM A1003 structural quality steel.
  • European Standard: EN 10346, EN 10149, and CE Marking execution standard EN 1090-2 (Execution Class EXC2 / EXC3).
  • Australasian Standard: AS/NZS 4600 and AS 1397 (G450, G500, G550 with Z275/AZ150 coatings).
  • Chinese National Standard: GB/T 6725, GB 50018, and GB/T 2518 (Q235B, Q355B).
Q4 Why is Zinc-Aluminum-Magnesium (Zn-Al-Mg) preferred over standard hot-dip galvanizing?
Zinc-Aluminum-Magnesium (ZM) alloy coatings outperform pure zinc (HDG) due to their dense, passive simonkolleite-based protective layer. When a ZM-coated purlin is cut, drilled, or punched, moisture induces an electrolytic reaction that causes magnesium and aluminum ions to migrate across the bare steel edge. This automatic self-healing mechanism seals the exposed carbon steel core, eliminating edge rust without expensive post-fabrication galvanizing or zinc-spray paint touch-ups.
Q5 What are the standard deflection limits for roof purlins and wall girts?
Deflection limits depend on the cladding material and design code:
  • Purlins supporting single-skin metal profile sheets: Maximum vertical live-load deflection typically capped at $L/180$ to $L/200$.
  • Purlins supporting insulated sandwich panels: Stricter limit of $L/240$ to $L/300$ to prevent joint separation and air leakage.
  • Wall girts under wind suction/pressure: Typically designed for horizontal lateral deflection not exceeding $L/150$ to $L/180$.
Q6 How do sag rods and lateral bridging prevent purlin twisting and failure?
Cold-formed thin-walled purlins are susceptible to lateral-torsional buckling under flexure because their shear center does not coincide with the center of gravity. Sag rods (tie rods) and diagonal apex bridging provide intermediate lateral and rotational restraint to the purlin's lower and upper flanges. Installing sag rods at mid-span or third-points cuts the unsupported span length, preserving the purlin's structural capacity under negative wind suction when the bottom flange goes into compression.
Q7 What dimensional ranges can your continuous roll-forming lines produce?
Our automated CNC lines can produce custom sizes across a wide envelope:
  • Web Depth (H): 80 mm up to 400 mm
  • Flange Width (B): 40 mm up to 120 mm (including unequal flanges for nesting)
  • Lip Return (C): 12 mm up to 30 mm (with 90° or 45° stiffener options)
  • Material Thickness (t): 1.2 mm up to 4.0 mm
  • Cut Length: Mill-cut to any custom transportable length up to 14.5 meters (for 45ft high-cube containers) or open-top flat racks.
Q8 How are purlin bundles packed to protect against sea moisture and physical damage?
Export shipments are packaged for rough maritime transit. Profiles are nested together to form solid, high-density blocks strapped with heavy-duty galvanized steel banding. The bundles are wrapped in waterproof VCI (Vapor Corrosion Inhibitor) plastic membranes, cushioned with perimeter steel corner edge protectors, and supported on grooved timber dunnage blocks suitable for direct forklift and crane sling offloading.
Q9 Can you provide custom-located pre-punched holes based on Tekla structural models?
Yes. We accept direct structural fabrication data (including Tekla .NC1 files, AutoCAD DWG layouts, and structural schedules). Our in-line hydraulic and servo punches automatically execute web holes, flange holes, and slotted thermal relief holes at precise coordinates during continuous forming. This eliminates on-site torch cutting, ensures clean galvanized margins, and allows for rapid erection using standard Grade 4.8 or 8.8 structural bolts.
Q10 What is the standard production lead time and export delivery capability?
Standard mill fabrication lead time is 10 to 18 days from technical drawing sign-off and LC establishment for volumes up to 500 metric tons. With multiple high-speed production lines operating simultaneously, we can process over 10,000 metric tons of secondary steel framing every month. Our proximity to major international shipping ports in China (Shanghai, Tianjin, Qingdao, Ningbo) enables weekly vessel sailings to worldwide destinations.
Direct Mill Engineering Consultation

Optimize Your Project's Secondary Steel Framing & Envelope Today

Submit your architectural blueprints, bay spacings, or Tekla purlin schedules. Our technical engineering division will generate comprehensive load-deflection calculations, optimized container nesting schemes, and competitive factory-direct pricing within 24 business hours.